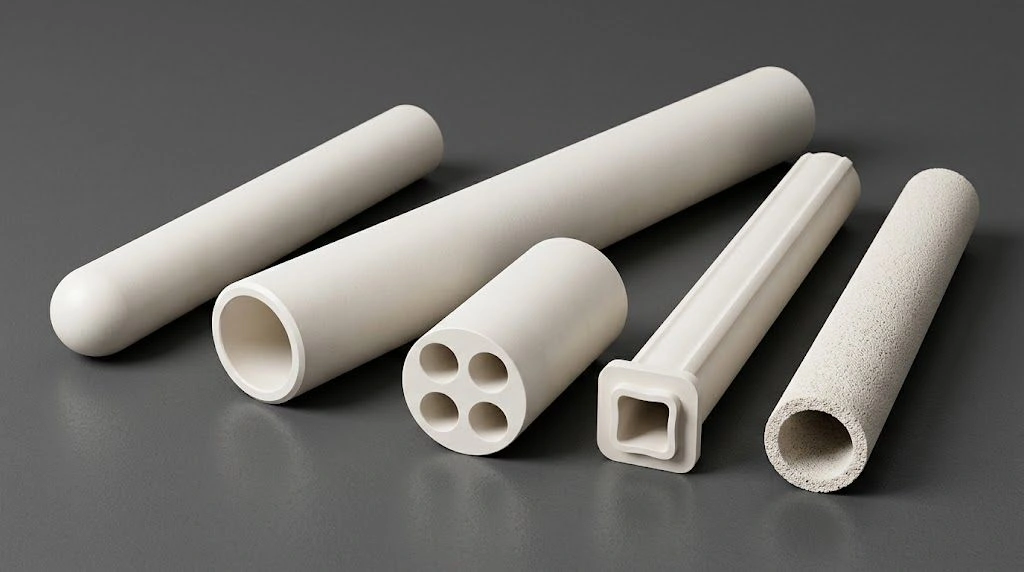
Alumina Thermocouple Protection Tubes are essential in high-temperature furnaces where thermocouples face corrosive, erosive, and chemically reactive atmospheres. Understanding how purity affects performance helps engineers prevent premature failure and improve measurement reliability above 1400°C.
Above 1400°C, grade selection typically pushes toward the ≥99.5% / 99.7% class — but purity alone does not “prevent” failure. Select by maximum temperature, furnace atmosphere (oxidizing / reducing / SO₂–alkali species), wall geometry, and lot SiO₂/alkali limits on the RFQ; confirm the ordered grade data sheet and duty. Performance still correlates with silica content, grain-boundary structure, and thermal strength retention under the actual atmosphere.
Selecting the correct alumina purity level requires analyzing degradation mechanisms, purity comparisons, and operational environments where performance differences become most significant. For tube sizes, closed-end options, and custom RFQ fields, see alumina tube sizes & custom RFQ. For a broader ceramic thermocouple-protection overview, see also ceramic thermocouple protection tubes for furnaces & reactors.

Understanding Degradation Mechanisms in Alumina Thermocouple Protection Tubes Above 1400°C
At furnace temperatures beyond 1400°C, alumina thermocouple protection tubes deteriorate through combined corrosion, erosion, and chemical interaction processes. These mechanisms progressively weaken structural integrity and lead to sensor failure.
Each degradation pathway has distinct causes and effects, influencing how long the tubes can maintain protective efficiency and dimensional stability under industrial conditions.
Corrosive Gas Attack Mechanisms on Grain Boundaries in High-Temperature Service
Corrosive gases such as sulfur dioxide (SO₂) react with alumina surfaces, forming volatile aluminum sulfate compounds that erode the protective layer. State SO₂/alkali species and dew point on the RFQ rather than treating any published corrosion-rate band as a contract corrosion curve. High-purity Alumina Thermocouple Protection Tubes resist this process because low silica content limits liquid-phase formation, helping maintain solid-state corrosion resistance when the duty and grade match.
Erosive Particle Impingement and Wall Thinning Rates in Particulate-Laden Atmospheres
In combustion systems, ash and oxide particles in high-velocity, particulate-laden gas streams impact tube surfaces, removing small amounts of material over time. Low-purity grades exhibit faster wall thinning due to weaker grain-boundary cohesion and higher porosity levels. Dense, high-purity tubes maintain smoother surfaces that limit particle retention and reduce cumulative erosive wear — validate under the actual gas velocity and particle loading.
Chemical Reaction Pathways Between Impurity Phases and Furnace Atmospheres
Residual silica in low-purity alumina forms silicate glass at temperatures above about 1200°C. This glassy network facilitates diffusion of corrosive gases, allowing deep structural penetration and internal oxidation. Driving silica down through higher-purity alumina compositions blocks this mechanism when lot chemistry is controlled, reducing surface pitting and internal porosity risk.
Comparing Alumina Thermocouple Protection Tubes by Purity Grades: 95%, 99%, 99.5%, 99.7%, and 99.9% Al₂O₃
Different purity levels of Alumina Thermocouple Protection Tubes determine their material-selection temperature ceiling and corrosion resistance. As impurity content decreases, the long-term temperature selection limit and chemical stability improve. Temperature ceilings below are initial material-selection limits — not permissible continuous temperatures for every load or atmosphere.
Selecting between standard and ultra-high-purity alumina depends on atmosphere composition, furnace type, and cost-performance balance.
Composition and Temperature Limits of Standard Furnace Grades (95–99%)
Lower-purity alumina grades carry more silica and alkali oxides than high-purity classes. These impurities form glassy phases that constrain practical service in corrosive sulfur or alkali vapors well below the clean-atmosphere selection ceiling. Such tubes can be economical in milder oxidizing duty, but fail more quickly when glassy grain-boundary networks open diffusion paths.
Performance Characteristics of Standard High-Purity Grades (99% Al₂O₃)
The 99% purity grade offers low total impurities when SiO₂ and alkali are controlled on the lot COA. Its long-term temperature selection ceiling is 1600°C on the grade sheet — still a selection limit, not a loaded-life rating in every atmosphere. In clean oxidizing environments it can be a practical choice; when SO₂ or alkali species are present, specify gas species and dew point on the RFQ and consider stepping purity up to limit glassy-phase formation.
Ultra-High-Purity Specifications and Elimination of Glassy Phase Formation
Ultra-high-purity alumina (≥99.5%, with 99.7% / 99.9% classes for higher ceilings) sharply reduces glassy phases. Grade-sheet long-term temperature selection ceilings reach 1650°C (99.50%), 1700°C (99.70%), and 1750°C (99.90%) — again as application ceilings, not guaranteed continuous service in every atmosphere. Uniform grain boundaries limit gas diffusion and resist both liquid-phase and solid-state corrosion when lot chemistry and duty match. Relative service life is plant-specific — not a contractual month count.
Alumina Thermocouple Protection Tubes: Purity Grade Performance Comparison
| Purity Grade | Long-term Temperature Selection Ceiling (°C) | Typical Impurity / Chemistry Note | Grain Boundary Glassy Phase | Relative Service Life in Corrosive Duty (orientation) | Relative Cost (orientation) |
|---|---|---|---|---|---|
| 95% Al₂O₃ | 1400 — selection ceiling; confirm atmosphere & load | Higher SiO₂ + oxides — specify max SiO₂/alkali on lot COA | Higher glassy fraction (qualitative) | Shorter vs higher-purity class — plant-specific, not contractual life | Lower |
| 99.00% Al₂O₃ | 1600 — selection ceiling; confirm atmosphere & load | Low total impurities — specify max SiO₂/alkali on lot COA / drawing | Lower glassy fraction vs 95% | Longer than 95% class in matching duty — plant-specific | Mid |
| 99.50% Al₂O₃ | 1650 — selection ceiling; confirm atmosphere & load | Tighter chemistry — specify max SiO₂/alkali on lot COA | Minimal glassy network when chemistry controlled | Longer than 99% class in matching duty — plant-specific | Higher |
| 99.70% Al₂O₃ | 1700 — selection ceiling; confirm atmosphere & load | Ultra-low SiO₂/alkali targets — confirm on lot COA | Near-elimination of glassy phase when chemistry controlled | Longer than 99.5% class in matching duty — plant-specific | Higher |
| 99.90% Al₂O₃ | 1750 — selection ceiling; confirm atmosphere & load | Tightest chemistry class on grade sheet — confirm lot COA | Minimal residual glassy phase | Longest orientation among listed classes — plant-specific, not contractual life | Highest |
Note: Temperature ceilings are initial material-selection limits, not permissible temperatures for every load or atmosphere. Relative life and cost columns are orientation only — quantify changeout interval and downtime on your plant model; they are not contractual life or TCO guarantees.
The Critical Role of High-Purity Alumina Thermocouple Protection Tubes (≥99.5% Al₂O₃) for Extreme Conditions
When furnace temperatures exceed 1400°C, ultra-high-purity Alumina Thermocouple Protection Tubes are typically preferred for stable thermocouple protection — provided atmosphere, geometry, and lot chemistry are specified together. Their microstructure limits corrosion pathways through silica control and reduces gas diffusion when glassy phases are minimized.
Engineering practice shows a strong qualitative correlation between purity class, silica control, and corrosion risk in aggressive atmospheres — reinforcing why >1400°C duty often moves the RFQ toward the ≥99.5% / 99.7% class after atmosphere and SiO₂ limits are stated.
Liquid Phase Formation Mechanisms and Temperature Dependencies in Alumina Systems
Elevated silica (specify a maximum on the lot COA / drawing rather than treating a fixed wt% threshold as a factory rule) can lead to liquid-phase formation in the roughly 1200–1400°C window. These molten phases act as conduits for SO₂ and alkali vapors, accelerating corrosion through grain boundaries. Ultra-high-purity alumina compositions prevent liquid-network development when chemistry is controlled, maintaining solid-state integrity.
Corrosion Resistance Enhancement Through Silica Content Minimization
Driving silica down (state a max SiO₂ and alkali limit on the lot COA / drawing) improves diffusion resistance and corrosion protection. Without glassy films, gases must diffuse through solid alumina — a much slower path than liquid diffusion. This physical barrier effect explains why ultra-pure Alumina Thermocouple Protection Tubes typically last longer in matching corrosive duty — still plant-specific, not a month-count guarantee.
Service-Life Comparison Across Purity Grades (Plant-Specific)
In high-temperature glass and similar furnace windows, higher-purity classes (e.g. 99.7%) typically outlast lower-purity tubes under the same atmosphere — but published month-to-month contrasts are not contractual life ratings. Confirm high-temperature flexural retention by an agreed HT method on the ordered grade and geometry rather than citing a fixed percent retention after a fixed soak. Purity remains a primary lever for reliability and measurement stability when atmosphere and chemistry are controlled.
Linking Low-Purity Alumina Thermocouple Protection Tubes to Specific Failure Mechanisms
Lower-purity Alumina Thermocouple Protection Tubes show characteristic degradation patterns caused by gas penetration and thermal mismatch. These mechanisms explain shorter operational campaigns in aggressive furnace conditions.
Each failure type reveals how impurity-driven reactions compromise structure and function during sustained high-temperature exposure.
Tube Bloating and Warping from Gas Penetration and Differential Expansion
Gas trapped within microvoids builds pressure, leading to bloating and tube expansion. Thermal expansion mismatch between the alumina matrix and silicate phases (alumina mean CTE ~7.6×10⁻⁶/K at 25–800°C on the grade sheet; 99.00% grade ~7.2) drives deformation and cracking when glassy phases are present. As deformation progresses, thermocouple alignment shifts, resulting in temperature measurement errors.
Accelerated Oxidation Mechanisms in Reducing Atmosphere Exposure
Reducing atmospheres with elevated hydrogen can promote reduction of silicate phases to volatile SiO gas. This reaction creates porosity and can reduce mechanical strength — confirm hydrogen species and strength retention by agreed duty testing rather than treating a fixed percent loss as a factory curve. High-purity alumina reduces this vulnerability by limiting silicate grain-boundary phases, helping maintain dense microstructure when the atmosphere is correctly specified.
Slag Penetration Pathways and Thermocouple Drift Progression
Molten slag infiltrates glassy grain boundaries through capillary action, contaminating the thermocouple junction. This can produce gradual calibration drift and eventual electrical failure — quantify acceptable drift on the RFQ rather than assuming a fixed °C band. Ultra-high-purity tubes resist slag ingress when glassy phases are minimized, preserving accuracy and stability over extended service cycles.
Selection Criteria for Alumina Thermocouple Protection Tubes: Balancing Purity, Cost, and Furnace Environment
Choosing the right Alumina Thermocouple Protection Tubes requires balancing purity grade, cost efficiency, and furnace atmosphere. Each application demands tailored solutions based on thermal and chemical conditions.
Lifecycle cost should be modeled from changeout interval and downtime — request grade, atmosphere species, and max temperature on the RFQ rather than assuming a fixed TCO percentage from purity alone.
Temperature and Atmosphere-Based Purity Selection Guidelines
For oxidizing atmospheres well below the 1600°C selection ceiling of the 99% class, 99% alumina can offer sufficient protection at moderate cost when SO₂/alkali are low. As temperature approaches or exceeds ~1400°C, or when corrosive gas species appear, step toward ≥99.5% (1650°C ceiling) or 99.7% / 99.9% classes (1700 / 1750°C ceilings) and state SO₂/alkali species and dew point on the RFQ. Above ~1500°C or in reducing/corrosive conditions, the 99.7% / 99.9% class is typically essential — confirm against the grade sheet and duty.
Economic Analysis of Purchase Cost Versus Service Life Trade-Offs
Higher-purity tubes cost more initially, but often lower changeout frequency in aggressive atmospheres. Quantify total cost on your downtime and replacement model rather than treating any fixed life-multiplier or TCO percentage as a factory guarantee. Downtime reductions and longer replacement intervals improve furnace uptime when the grade matches the atmosphere.
Special Considerations for Reducing Atmospheres and Thermal Cycling Applications
Frequent temperature cycles with large differentials can fatigue standard sintered alumina. Recrystallized alumina structures are often preferred for thermal-shock-heavy duty regardless of purity class — treat recrystallized vs sintered as a structural option to confirm on the drawing. Continuous processes without large temperature swings can use standard sintered forms when cost optimization matters and thermal-shock qualification is not the limiter.
Closed-end and furnace-tube geometries (OD/ID/wall, insertion length) should be confirmed against duty; see alumina furnace / protection tube geometries when the RFQ needs a specific closed-end or furnace-tube form factor.
Alumina Thermocouple Protection Tube Selection Decision Matrix
| Operating Condition | Recommended Purity | Key Reason |
|---|---|---|
| 1200–1300°C, oxidizing, low SO₂/alkali (state species on RFQ) | 99% Al₂O₃ | Economical and stable for clean atmospheres within 1600°C selection ceiling |
| ~1300–1500°C or mildly corrosive gas (state SO₂/alkali & dew point on RFQ) | ≥99.5% Al₂O₃ | Limits glassy-phase formation; 1650°C selection ceiling |
| >1500°C or reducing/corrosive conditions | 99.7% / 99.9% Al₂O₃ class | Higher selection ceilings (1700 / 1750°C) and stronger corrosion margin when chemistry controlled |
| High thermal cycling (large ΔT; confirm cycle count on RFQ) | Recrystallized structure (any matching purity) | Improves thermal-shock resistance as a structural option |
RFQ checklist (short)
- Maximum continuous / peak temperature (°C)
- Atmosphere gases (oxidizing / reducing / SO₂ / alkali species) and dew point if relevant
- Thermal cycle count and ΔT
- OD / ID / wall thickness and length
- Closed-end vs open-end; insertion length
- Max SiO₂ (and alkali) on lot COA / drawing
- Quantity and required certifications
Conclusion
For furnace atmospheres above 1400°C, step alumina thermocouple protection tubes toward the ≥99.5% / 99.7% (or 99.9%) class only after temperature, atmosphere species, geometry, and lot chemistry are stated together — purity is a primary lever against corrosion, slag attack, and measurement drift, not a standalone guarantee.
Send Tmax, atmosphere gases (incl. SO₂/alkali if any), OD/ID/wall, closed/open end, cycle ΔT, and max SiO₂ on COA for a neutral purity×atmosphere RFQ checklist review against the ordered grade data sheet and duty — no catalog commitment required at this stage.
FAQ
Q1: How does alumina purity affect performance in furnace atmospheres above 1400°C?
Alumina Thermocouple Protection Tubes with higher purity resist liquid-phase corrosion and typically provide longer service life due to reduced silica activity — when atmosphere and lot chemistry are controlled. Confirm grade-sheet selection ceiling and duty together.
Q2: Are high-purity alumina tubes worth the additional cost?
Often yes in aggressive atmospheres: higher-purity classes can lower changeout frequency and downtime. Quantify lifecycle cost on your replacement interval and downtime model rather than assuming a fixed TCO percentage.
Q3: Can custom dimensions be produced for specialized applications?
Custom diameters, lengths, and closed-end configurations are routinely specified — send OD/ID/wall, length, atmosphere, and max temperature on the RFQ.
Q4: How do alumina tubes compare to silicon carbide or mullite alternatives?
Alumina provides strong chemical inertness and electrical insulation for thermocouple protection in many harsh furnace atmospheres. SiC or mullite may fit other thermal-shock or conductivity duties — choose by atmosphere, temperature, and measurement requirements rather than a single material default.
Related reading
- Alumina protection tubes for lab furnaces: spec logic — Spec OD/ID, closed end, and insertion length before you freeze an alumina grade.
- Alumina protection tubes in cement kiln preheaters — Protection-tube duty in cement kiln preheater gas streams and alkali dust.
- Alumina tubes for glass-melting temperature monitoring — Alumina tube choices when the job is glass-furnace temperature monitoring.