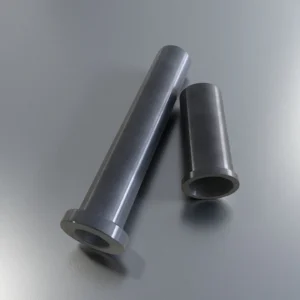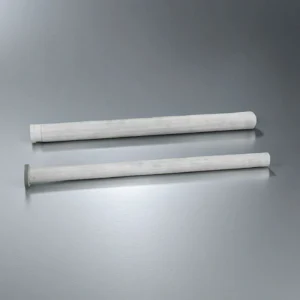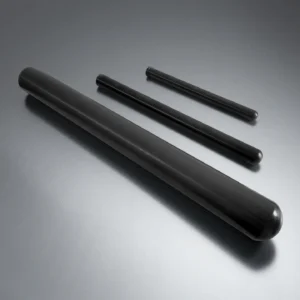
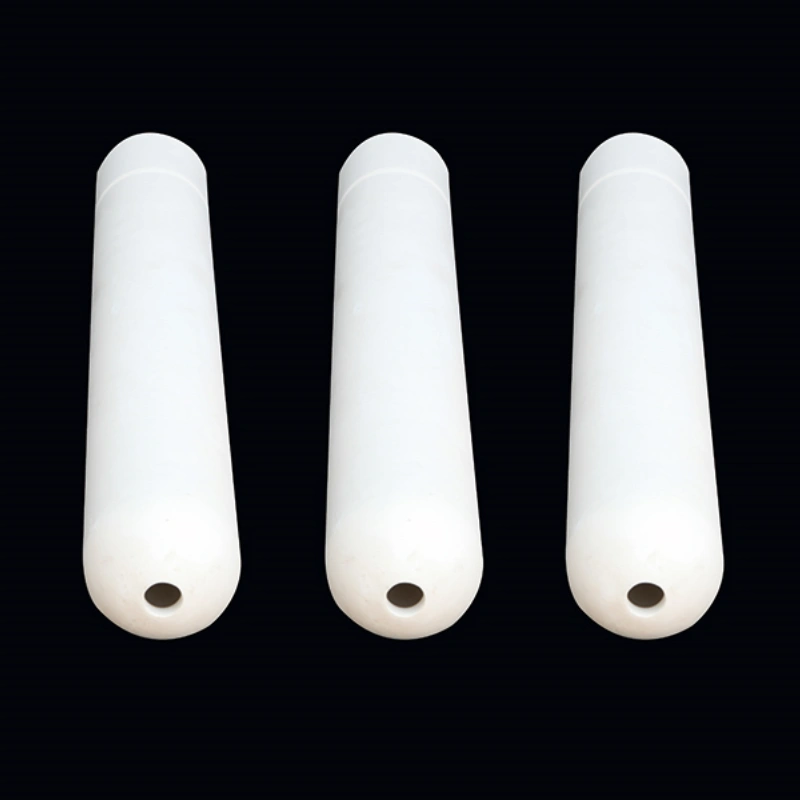
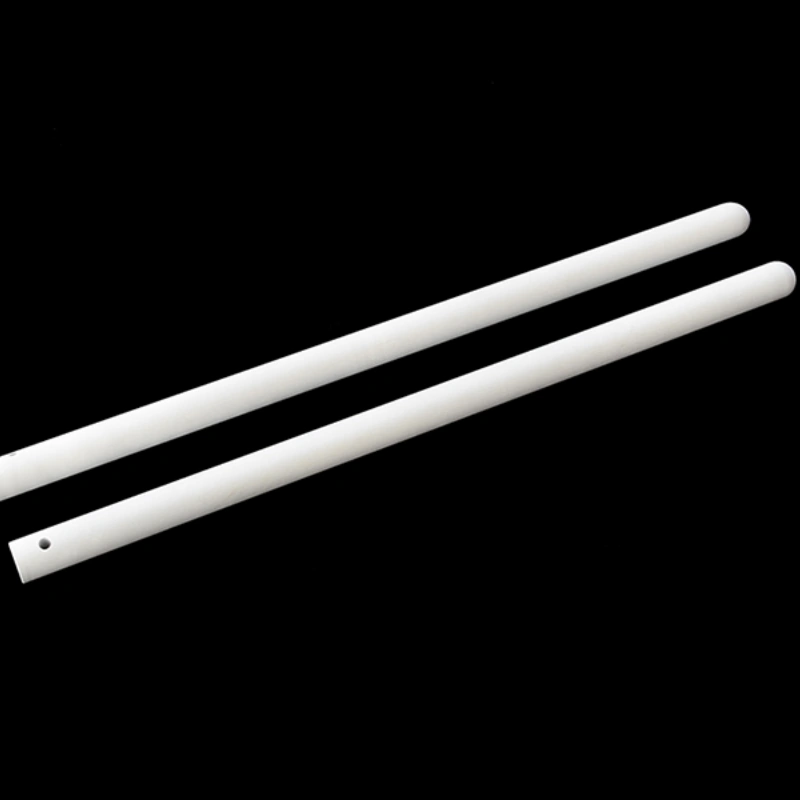
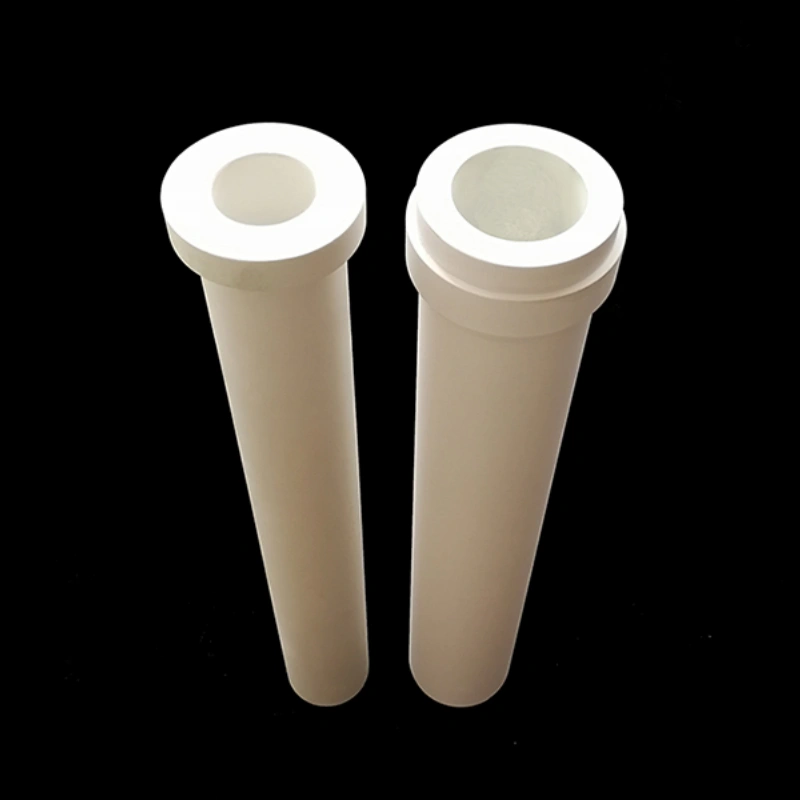
Aluminum Titanate Riser Tube for Low-Pressure Aluminium Casting

Aluminum titanate (Al₂TiO₅) helps LPDC riser tubes limit thermal cracking, aluminum build-up and heat loss. ADCERAX supports typical reference sizes of about 40–120 mm ID and lengths up to around 1500 mm, with ID, OD, total length, immersion depth and flange geometry customized after drawing and operating-condition review.

Catalogue No. AT-TSL-SYG1001
Material Aluminum Titanate (Al₂TiO₅)
Thermal Conductivity ~1–2 W/m·K
Coefficient of Thermal Expansion ~1–2 × 10⁻⁶ K⁻¹ (20–1000 °C)
Recommended Service Temperature Designed for molten-aluminum service, typically ~700–900 °C; higher only by grade and engineering confirmation
Engineering RFQ Review
Small-Batch Custom Support
Factory-Direct Manufacturing
Drawing & Process Review

An aluminum titanate (Al2TiO5) riser tube — also called a stalk tube — is the ceramic channel that lifts molten aluminum from a holding or dosing furnace into the die in low-pressure die casting (LPDC). It combines very low thermal expansion, thermal-shock resistance, low thermal conductivity and a surface that molten aluminum does not wet, so it can run repeated 700–900 °C casting cycles with less cracking, less metal sticking and steadier metal flow than steel or cast-iron stalks.

Aluminum Titanate Riser Tube Benefits

  • Low thermal expansion for thermal cycling — near-zero CTE helps the tube take repeated room-to-≥700 °C cycles with less thermal-stress cracking.
  • Non-wetting to molten aluminum — the bore is not wetted by aluminum, so it resists sticking and dross build-up and helps keep the melt clean.
  • Low thermal conductivity — limits heat loss along the metal column, supporting steady melt temperature and mold filling.
  • Cleaner metal flow, less slag build-up — low conductivity plus non-wetting help reduce slag at the top of the riser, supporting more consistent casting quality.
  • Thermal-shock resistant, often without pre-heating — good thermal-shock behavior can reduce pre-heating effort before installation.
  • Service life suited to continuous LPDC — matched to the alloy, furnace temperature and cycle, it can give a useful working life that reduces tube changes.

Aluminum Titanate vs Sialon vs Steel Riser Tubes

Selecting a riser-tube material depends on the molten alloy, furnace temperature, pressure cycle, mechanical loading and current failure mode. The comparison below provides an initial engineering reference.

Aluminum Titanate (Al₂TiO₅)

Key advantages: Very low thermal expansion, low wettability by molten aluminum and low thermal conductivity.

Main consideration: Brittle ceramic requiring careful handling and even flange loading.

Typical fit: LPDC and dosing systems where thermal cycling, aluminum build-up and heat loss are key concerns.

Sialon / Silicon Nitride (Si₃N₄)

Key advantages: Higher mechanical strength with good wear and thermal-shock resistance.

Main consideration: Grade, interface design and project cost require separate evaluation.

Typical fit: Systems where mechanical loading and structural durability are priorities.

Steel or Cast-Iron Stalk

Key advantages: High mechanical strength and familiar fabrication.

Main consideration: May require coatings and maintenance to manage aluminum wetting, corrosion, thermal fatigue and heat loss.

Typical fit: Existing systems where mechanical robustness and conventional replacement practices are preferred.

Aluminum Titanate Riser Tube Properties

Parameter Typical Value Description
Coefficient of Thermal Expansion (CTE) 0.5–1.5 ×10⁻⁶ /K Extremely low expansion that maintains dimensional stability under molten aluminum temperatures.
Thermal Shock Resistance Very high Withstands rapid temperature fluctuations without cracking during casting cycles.
Density 2.8–3.0 g/cm³ Medium-density ceramic structure suitable for molten aluminum system components.
Thermal Conductivity 1–2 W/m·K Helps reduce heat loss along riser tubes, spouts and transfer components.
Maximum Service Temperature Molten-aluminum service typ. 700–900 °C Suitable for typical molten-aluminum environments and transfer systems.
Flexural Strength (MOR) 10–25 MPa Provides sufficient strength for handling, installation and operational load.
Elastic Modulus 20–40 GPa Lower stiffness contributes to excellent thermal shock tolerance.
Porosity 12–25% Supports insulation and limits internal thermal stress accumulation.
Chemical Compatibility Non-wetting to molten aluminum Prevents adhesion, oxide buildup and contamination in casting processes.
Dimensional Stability Stable through long cycles Maintains geometry during prolonged molten-aluminum exposure and thermal cycling.

Aluminum Titanate Riser Tube Specifications

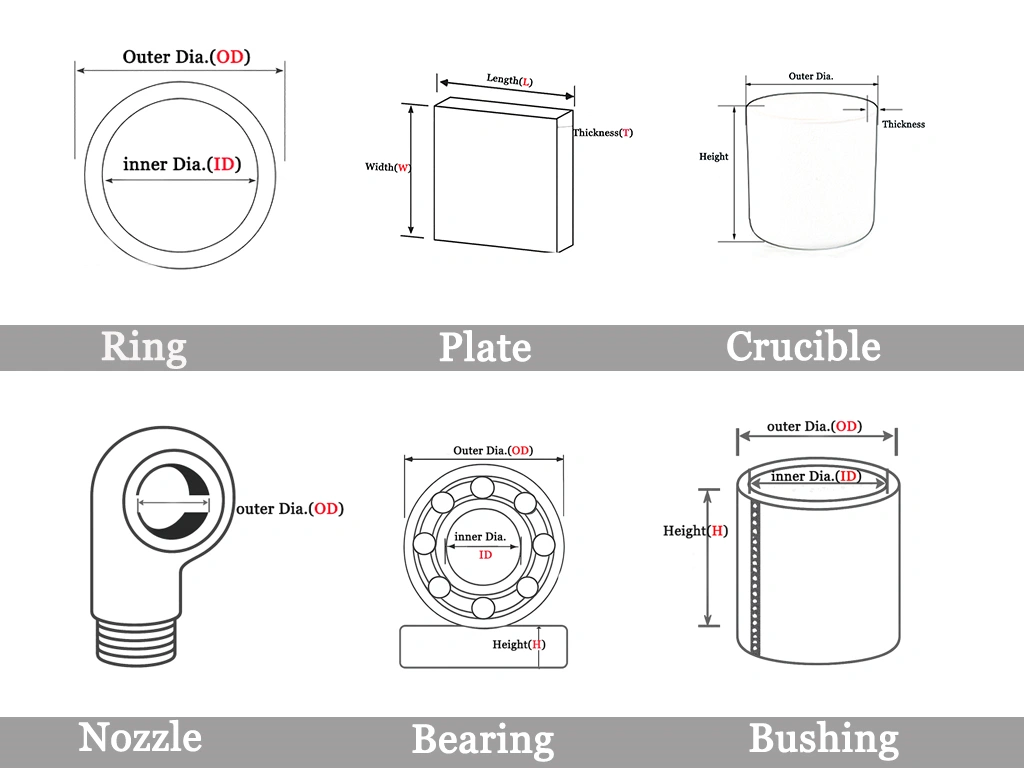
Item Outer Dia (mm) Inner Dia (mm) Length (mm)
AT-TSL-SYG1001 78 58 850
AT-TSL-SYG1002 90 61 850
AT-TSL-SYG1003 100 80 400
AT-TSL-SYG1004 100 60 900
AT-TSL-SYG1005 100 60 970
AT-TSL-SYG1006 105 75 1050
AT-TSL-SYG1007 110 63.5 900
AT-TSL-SYG1008 114 68 1100
AT-TSL-SYG1009 120 100 600
AT-TSL-SYG1010 120 100 800
AT-TSL-SYG1011 120 70 1220
AT-TSL-SYG1012 120 80 950
AT-TSL-SYG1013 120 80 930
AT-TSL-SYG1014 130 110 1063
AT-TSL-SYG1015 130 100 750

Aluminium Titanate Riser Tube Packaging

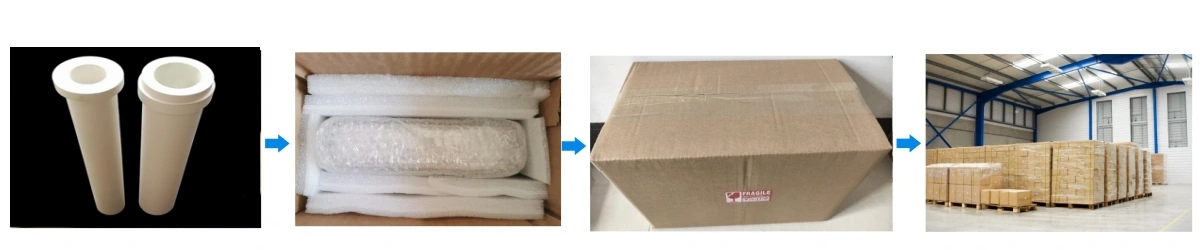
  • Each Aluminum Titanate Riser Tube is wrapped in shock-absorbing material (foam or soft padding) to protect ceramic surfaces from impact during transport
Aluminium Titanate Riser Tube Packaging

Application Scenarios – Aluminium Titanate Riser Tube

  • Automotive Aluminum Wheel and Chassis LPDC Lines – Key Advantages of Aluminum Titanate Riser Tube

    ✅Key Advantages

    Aluminum Titanate Riser Tube keeps low thermal expansion and non-wetting behavior in 700–900 °C molten aluminum, helping low-pressure die casting machines deliver metal to wheel molds in a consistent flow pattern.

    ✅ Problem Solved

    Automotive aluminum wheel LPDC lines — Steel or non-optimized ceramic stalks can cause turbulence, oxide generation and cracking over continuous cycles, adding scrap and unplanned stops. Aluminum titanate riser tubes typically reduce metal adhesion and improve thermal-shock life, which can help one tube cover more casting cycles between changes

  • Non-Ferrous Aluminum Foundries and Alloy Casting Shops – Key Advantages of Aluminum Titanate Riser Tube

    ✅Key Advantages

    Aluminum Titanate Riser Tube presents a surface that is not wetted by molten aluminum, limiting oxide skins and metal build-up along the internal bore, which supports cleaner aluminum alloy castings with fewer inclusions.

    ✅ Problem Solved

    Non-ferrous aluminum foundries — Long campaigns with wetted stalks tend to cause internal build-up and dross carryover. By resisting wetting, aluminum titanate riser tubes help maintain a stable effective bore and can reduce cleaning and replacement frequency, supporting more consistent metal quality.

  • LPDC Equipment OEMs and Dosing Furnace Builders – Key Advantages of Aluminum Titanate Riser Tube

    ✅  Key Advantages

    Aluminum Titanate Riser Tube combines low thermal expansion, low thermal conductivity and sufficient mechanical integrity, allowing equipment OEMs to integrate the stalk with dosing furnaces and molds as part of a controlled thermal system.

    ✅  Problem Solved

    LPDC equipment OEMs & dosing-furnace builders — Used as a standard stalk, aluminum titanate helps OEMs offer a controlled-thermal-loss solution that supports longer campaigns and more predictable maintenance planning (matched to alloy, temperature and cycle).


Product Usage Guide – Aluminum Titanate Riser Tube

  • Handling & care

    Aluminum titanate has excellent thermal-shock resistance but relatively low mechanical strength. Handle and transport with impact protection, keep the tube dry before installation, seat and tighten the flange evenly (never over-torque or off-center), follow a controlled pre-heat curve on first heat-up, and clean slag with soft tools without striking the tube.

  • Installation

    1. Verify that the aluminum titanate riser tube dimensions, flange pattern and sealing surfaces match the low-pressure die casting or dosing furnace design before installation.
    2. Inspect the tube visually for cracks, chips or impact damage before mounting; do not install damaged riser tubes.
    3. Align the riser tube vertically according to the reference marks, so that immersion depth and flange contact surfaces match the design position.
    4. Use the specified gaskets and tightening sequence for bolts to ensure uniform flange compression and gas-tight sealing.

  • Operation

    1. During first heat-up, raise furnace and molten aluminum temperature gradually according to the line’s preheating curve, so that the aluminum titanate riser tube warms evenly.
    2. Maintain aluminum melt temperature within the recommended casting range (typically around 700–750 °C for many alloys) and avoid rapid temperature fluctuations where possible.
    3. Monitor pressure cycles and ensure that the low-pressure casting machine operates within the designed pressure and time profile for the riser tube.
    4. Avoid mechanical shock from tooling, tools or handling equipment near the stalk during operation.

  • Storage

    1. Store aluminum titanate riser tubes in a dry, clean indoor area, away from direct impact or vibration.
    2. Keep tubes in original crates or on cushioned racks, with supports located near the flange and at intermediate points for long tubes.
    3. Protect from water or oil contamination that could enter the open bore and affect behavior during first heat-up.

  • Cleaning and Inspection

    1. Do not mechanically scrape the inner bore aggressively; if surface build-up appears, use soft tools or controlled blasting methods recommended for ceramic components.
    2. Inspect riser tubes at planned intervals for signs of cracking, spalling, severe erosion or loss of cross-section.
    3. Replace tubes if cracking reaches sealing areas or if the internal bore cross-section is significantly reduced.

  • Common Misuse Points and Suggested Fixes

    1. Rapid temperature ramp from ambient to molten aluminum contact
    Misuse: charging cold aluminum titanate riser tubes directly into a hot furnace or molten aluminum environment.
    Fix: follow controlled preheating steps with pre-drying and gradual temperature increase, as specified by the furnace and tube supplier.

    2. Over-tightening or uneven tightening of flange bolts
    Misuse: excessive torque on individual bolts leading to flange edge cracking.
    Fix: tighten bolts in a cross pattern with specified torque, and use suitable gaskets to distribute load.

    3. Using damaged riser tubes after visible impact
    Misuse: installing tubes with visible chips or hairline cracks after transport or maintenance.
    Fix: quarantine suspect tubes, perform inspection, and replace if any structural crack is detected in critical sections.

FAQ – Aluminium Titanate Riser Tube

  1. Q: What is an Aluminum Titanate Riser Tube in low-pressure die casting?
    A: Aluminum Titanate Riser Tube is an Al₂TiO₅ ceramic stalk used in low-pressure die casting machines to lift molten aluminum from the holding or dosing furnace into the mold cavity under controlled gas pressure.
  2. Q: Why choose an Aluminum Titanate Riser Tube instead of a steel stalk?
    A: An aluminum titanate riser tube offers a much lower thermal expansion coefficient, better thermal shock resistance and non-wetting behavior with molten aluminum than steel, which reduces cracking, metal contamination and frequent replacement.
  3. Q: What temperature range can an Aluminum Titanate Riser Tube handle?
    Aluminum titanate riser tubes are designed for molten aluminum applications around 700–900 °C and can be used up to about 1200 °C in service, with short-term exposure reported up to around 1400 °C depending on the grade and design.
  4. Q: How long does an Aluminum Titanate Riser Tube typically last in LPDC operation?
    Service life depends on alloy, cycle time and furnace operation, but aluminum titanate riser tubes are intended to withstand many thermal cycles in LPDC lines, often significantly exceeding the life of steel stalks under comparable conditions.
  5. Q: Is an Aluminum Titanate Riser Tube compatible with different aluminum alloys?
    A: Yes. Aluminum titanate riser tubes are used across common aluminum casting alloys and are selected for their non-wetting and corrosion-resistant behavior with molten aluminum and other non-ferrous alloys.
  6. Q: Can the Aluminum Titanate Riser Tube be customized for my LPDC machine?
    A: Aluminum titanate riser tubes can be customized in ID, OD, length, flange style, bolt patterns and immersion depth to fit existing low-pressure die casting machines and dosing furnaces without modifying the core equipment.
  7. Q: Aluminum titanate vs Sialon (Si3N4) riser tube — which should I choose?
    A: Aluminum titanate is chosen for very low thermal expansion, non-wetting behavior toward molten aluminum and low thermal conductivity, often with little pre-heating. Sialon/silicon nitride is a higher-strength, long-life route at higher cost. The best fit depends on your alloy, furnace temperature, cycle and budget — send your conditions and we'll help compare.
  8. Q: Why do riser tubes stick aluminum or crack, and how does aluminum titanate help?
    A: Metal stalks are wetted by aluminum (sticking, dross) and fatigue under thermal cycling (cracking). Aluminum titanate resists wetting and has very low thermal expansion, so it typically reduces sticking and thermal-stress cracking — though it must be handled carefully because its mechanical strength is relatively low.
  9. Q: What information do you need to quote a custom riser tube?
    A: Old-part photos and failure mode, OD/ID/wall/length, immersion depth, flange type and bolt pattern, sealing face, casting machine model, aluminum alloy, furnace temperature and cycle, plus quantity. With these our engineers confirm manufacturability and typical lead time.
customize size

Custom Aluminum Titanate Riser Tubes

ADCERAX customizes aluminum titanate riser tubes to match existing LPDC machines, aluminum wheel casting lines and dosing furnaces.

1. Dimensions

  • Inner diameter (ID): approximately 40–120 mm or based on the existing stalk design
  • Outer diameter (OD) and wall thickness based on structural and flow requirements
  • Overall length: typically up to approximately 1500 mm
  • Immersion depth and non-immersed sections

2. End and Flange Designs

  • T-flange, bulk flange or custom geometry for the existing sealing surface
  • Open, tapered or specially shaped bottom end
  • Custom bolt-hole pattern, gasket groove and sealing face

3. Connection and Interface Details

  • Interface with the launder, dosing furnace or filter-box inlet
  • Integration with sprue bushings, filters or launder spouts

4. Material Options

  • Aluminum titanate grades for molten-aluminum contact
  • Grade selection based on thermal cycling and operating conditions

5. Inspection and Marking

  • Specified dimensional inspection points and tolerance requirements
  • Batch and installation-orientation marking when required

Related Products

ADCERAX - Your Trusted Advanced Ceramics Manufacturing Partner

Direct factory manufacturing with comprehensive ceramic materials expertise and global supply capabilities

China-Based Manufacturer

ADCERAX supplies ceramic components for overseas OEMs, equipment builders, and labs.

Custom Drawing Support

We review drawings, dimensions, materials, and application conditions before quotation.

Ceramic Process Control

Forming, sintering, machining, grinding, and finishing are arranged by part requirements.

Pre-Shipment Inspection

Dimensional checks, visual inspection, and packaging review help reduce procurement risk.

Get in Touch with Us

Our team will be happy to respond to you in less than 24 hours.

Pingxiang Factory — Silicon carbide, silicon nitride, high-temperature ceramics

Quick Quotation

*Our team will answer your inquiries within 24 hours.

*Your information will be kept strictly confidential.

Ready to Solve Your Engineering Challenge?

Partner with ADCERAX for reliable, high-performance advanced ceramic solutions. Our engineers are ready to discuss your project.

E-mail

info@adcerax.com

Phone

Tel: +86-0731-84428843 WhatsApp: +86 19311583352

Response Time

Within 24 hours

An aluminum titanate (Al2TiO5) riser tube — also called a stalk tube — is the ceramic channel that lifts molten aluminum from a holding or dosing furnace into the die in low-pressure die casting (LPDC). It combines very low thermal expansion, thermal-shock resistance, low thermal conductivity and a surface that molten aluminum does not wet, so it can run repeated 700–900 °C casting cycles with less cracking, less metal sticking and steadier metal flow than steel or cast-iron stalks.

Aluminum Titanate Riser Tube Benefits

  • Low thermal expansion for thermal cycling — near-zero CTE helps the tube take repeated room-to-≥700 °C cycles with less thermal-stress cracking.
  • Non-wetting to molten aluminum — the bore is not wetted by aluminum, so it resists sticking and dross build-up and helps keep the melt clean.
  • Low thermal conductivity — limits heat loss along the metal column, supporting steady melt temperature and mold filling.
  • Cleaner metal flow, less slag build-up — low conductivity plus non-wetting help reduce slag at the top of the riser, supporting more consistent casting quality.
  • Thermal-shock resistant, often without pre-heating — good thermal-shock behavior can reduce pre-heating effort before installation.
  • Service life suited to continuous LPDC — matched to the alloy, furnace temperature and cycle, it can give a useful working life that reduces tube changes.

Aluminum Titanate vs Sialon vs Steel Riser Tubes

Selecting a riser-tube material depends on the molten alloy, furnace temperature, pressure cycle, mechanical loading and current failure mode. The comparison below provides an initial engineering reference.

Aluminum Titanate (Al₂TiO₅)

Key advantages: Very low thermal expansion, low wettability by molten aluminum and low thermal conductivity.

Main consideration: Brittle ceramic requiring careful handling and even flange loading.

Typical fit: LPDC and dosing systems where thermal cycling, aluminum build-up and heat loss are key concerns.

Sialon / Silicon Nitride (Si₃N₄)

Key advantages: Higher mechanical strength with good wear and thermal-shock resistance.

Main consideration: Grade, interface design and project cost require separate evaluation.

Typical fit: Systems where mechanical loading and structural durability are priorities.

Steel or Cast-Iron Stalk

Key advantages: High mechanical strength and familiar fabrication.

Main consideration: May require coatings and maintenance to manage aluminum wetting, corrosion, thermal fatigue and heat loss.

Typical fit: Existing systems where mechanical robustness and conventional replacement practices are preferred.

Aluminum Titanate Riser Tube Properties

Parameter Typical Value Description
Coefficient of Thermal Expansion (CTE) 0.5–1.5 ×10⁻⁶ /K Extremely low expansion that maintains dimensional stability under molten aluminum temperatures.
Thermal Shock Resistance Very high Withstands rapid temperature fluctuations without cracking during casting cycles.
Density 2.8–3.0 g/cm³ Medium-density ceramic structure suitable for molten aluminum system components.
Thermal Conductivity 1–2 W/m·K Helps reduce heat loss along riser tubes, spouts and transfer components.
Maximum Service Temperature Molten-aluminum service typ. 700–900 °C Suitable for typical molten-aluminum environments and transfer systems.
Flexural Strength (MOR) 10–25 MPa Provides sufficient strength for handling, installation and operational load.
Elastic Modulus 20–40 GPa Lower stiffness contributes to excellent thermal shock tolerance.
Porosity 12–25% Supports insulation and limits internal thermal stress accumulation.
Chemical Compatibility Non-wetting to molten aluminum Prevents adhesion, oxide buildup and contamination in casting processes.
Dimensional Stability Stable through long cycles Maintains geometry during prolonged molten-aluminum exposure and thermal cycling.

Aluminum Titanate Riser Tube Specifications

Item Outer Dia (mm) Inner Dia (mm) Length (mm)
AT-TSL-SYG1001 78 58 850
AT-TSL-SYG1002 90 61 850
AT-TSL-SYG1003 100 80 400
AT-TSL-SYG1004 100 60 900
AT-TSL-SYG1005 100 60 970
AT-TSL-SYG1006 105 75 1050
AT-TSL-SYG1007 110 63.5 900
AT-TSL-SYG1008 114 68 1100
AT-TSL-SYG1009 120 100 600
AT-TSL-SYG1010 120 100 800
AT-TSL-SYG1011 120 70 1220
AT-TSL-SYG1012 120 80 950
AT-TSL-SYG1013 120 80 930
AT-TSL-SYG1014 130 110 1063
AT-TSL-SYG1015 130 100 750

Aluminium Titanate Riser Tube Packaging

  • Each Aluminum Titanate Riser Tube is wrapped in shock-absorbing material (foam or soft padding) to protect ceramic surfaces from impact during transport
Aluminium Titanate Riser Tube Packaging

Quick Quote

The more details you provide, the faster we can quote.

*All inquiries are confidential.

Get Your Custom Solution

The more details you provide, the faster we can respond.

customize size

*We respond within 24 hours. All inquiries are confidential.

Download Catalog