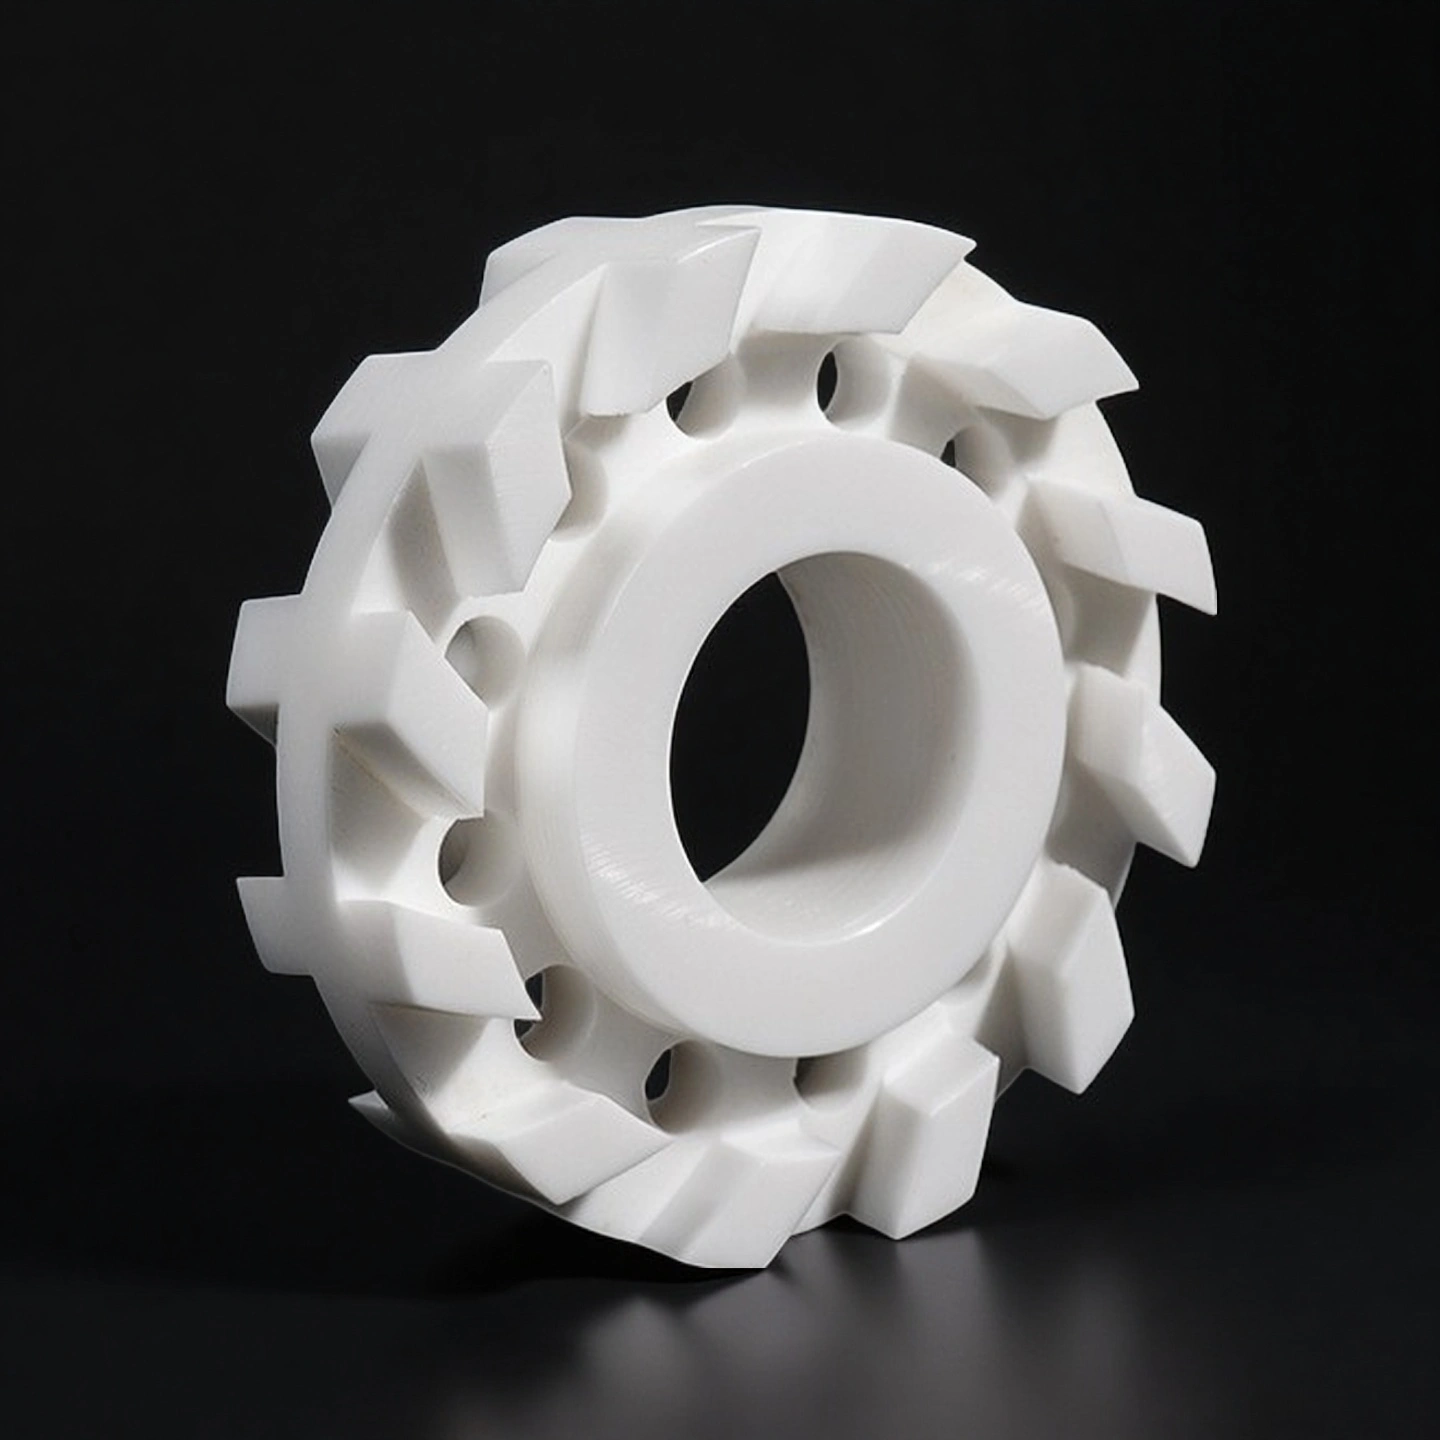
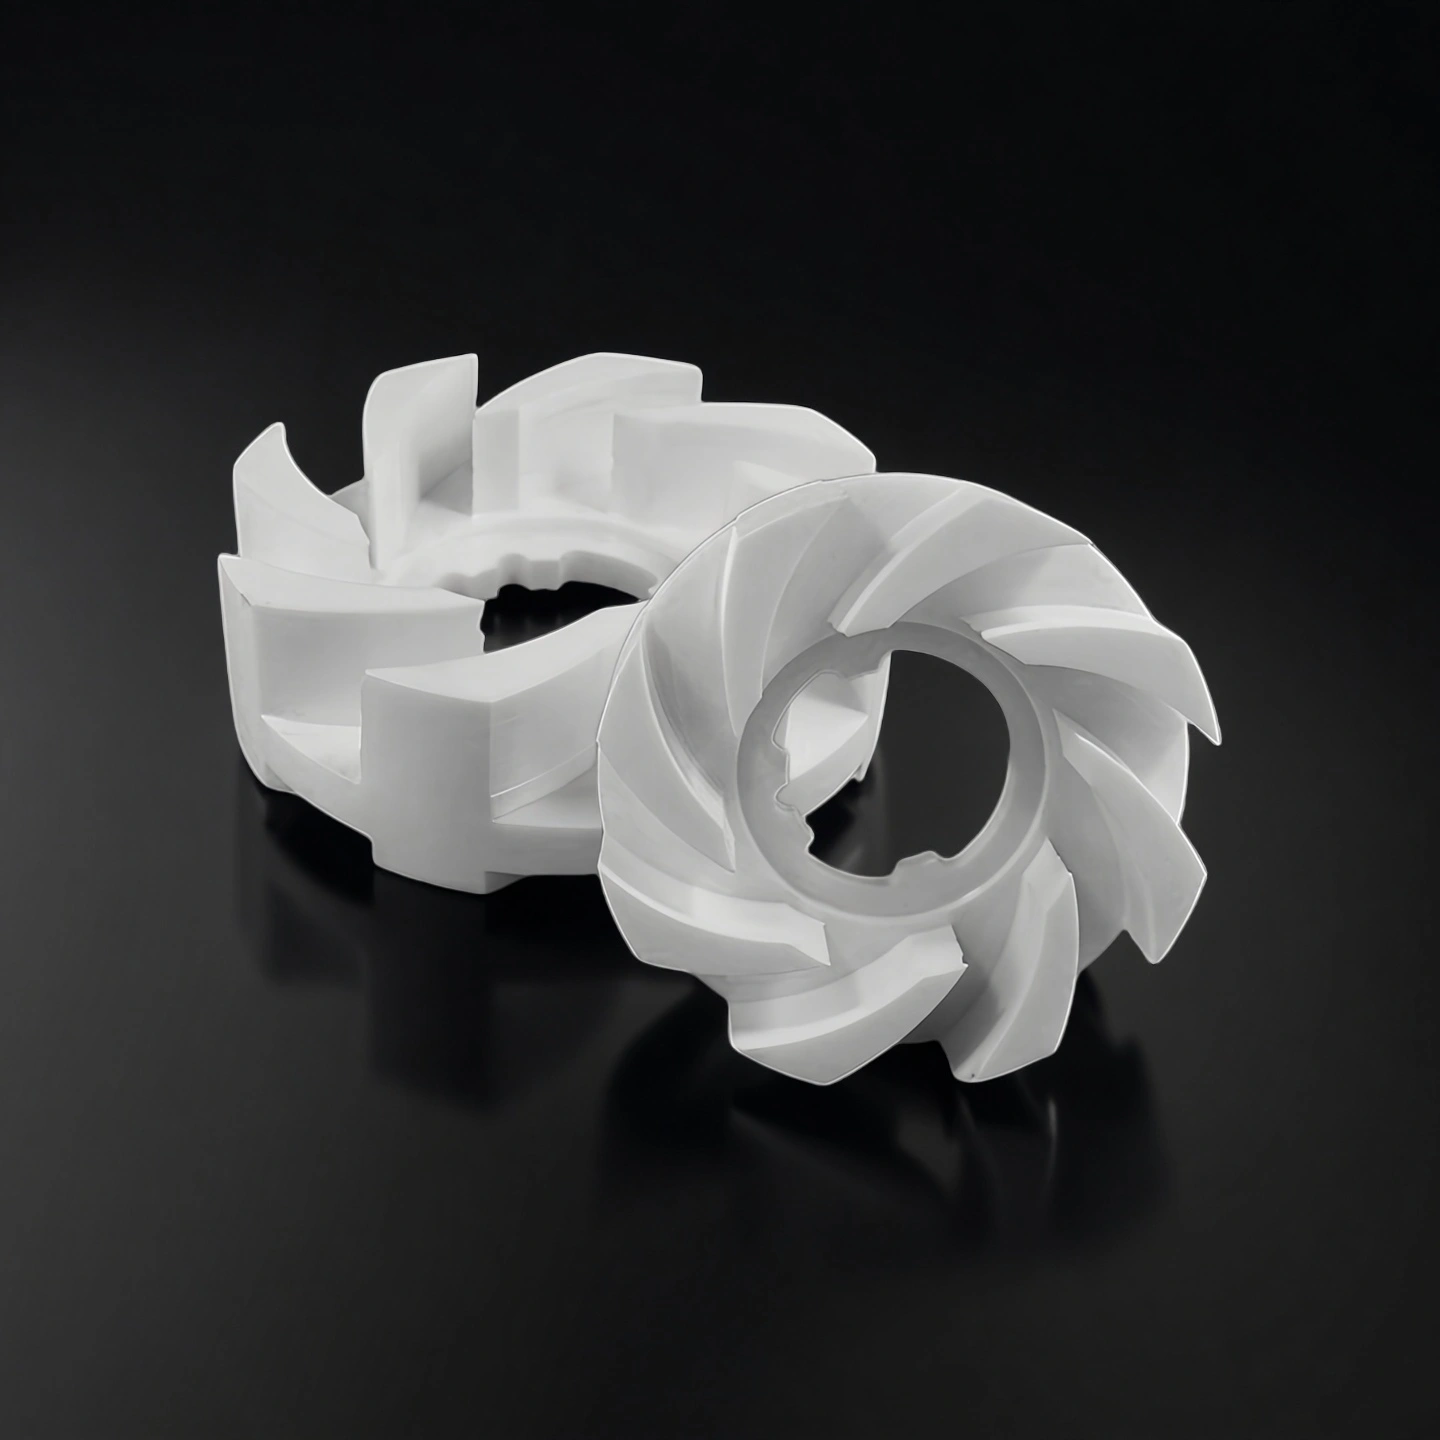
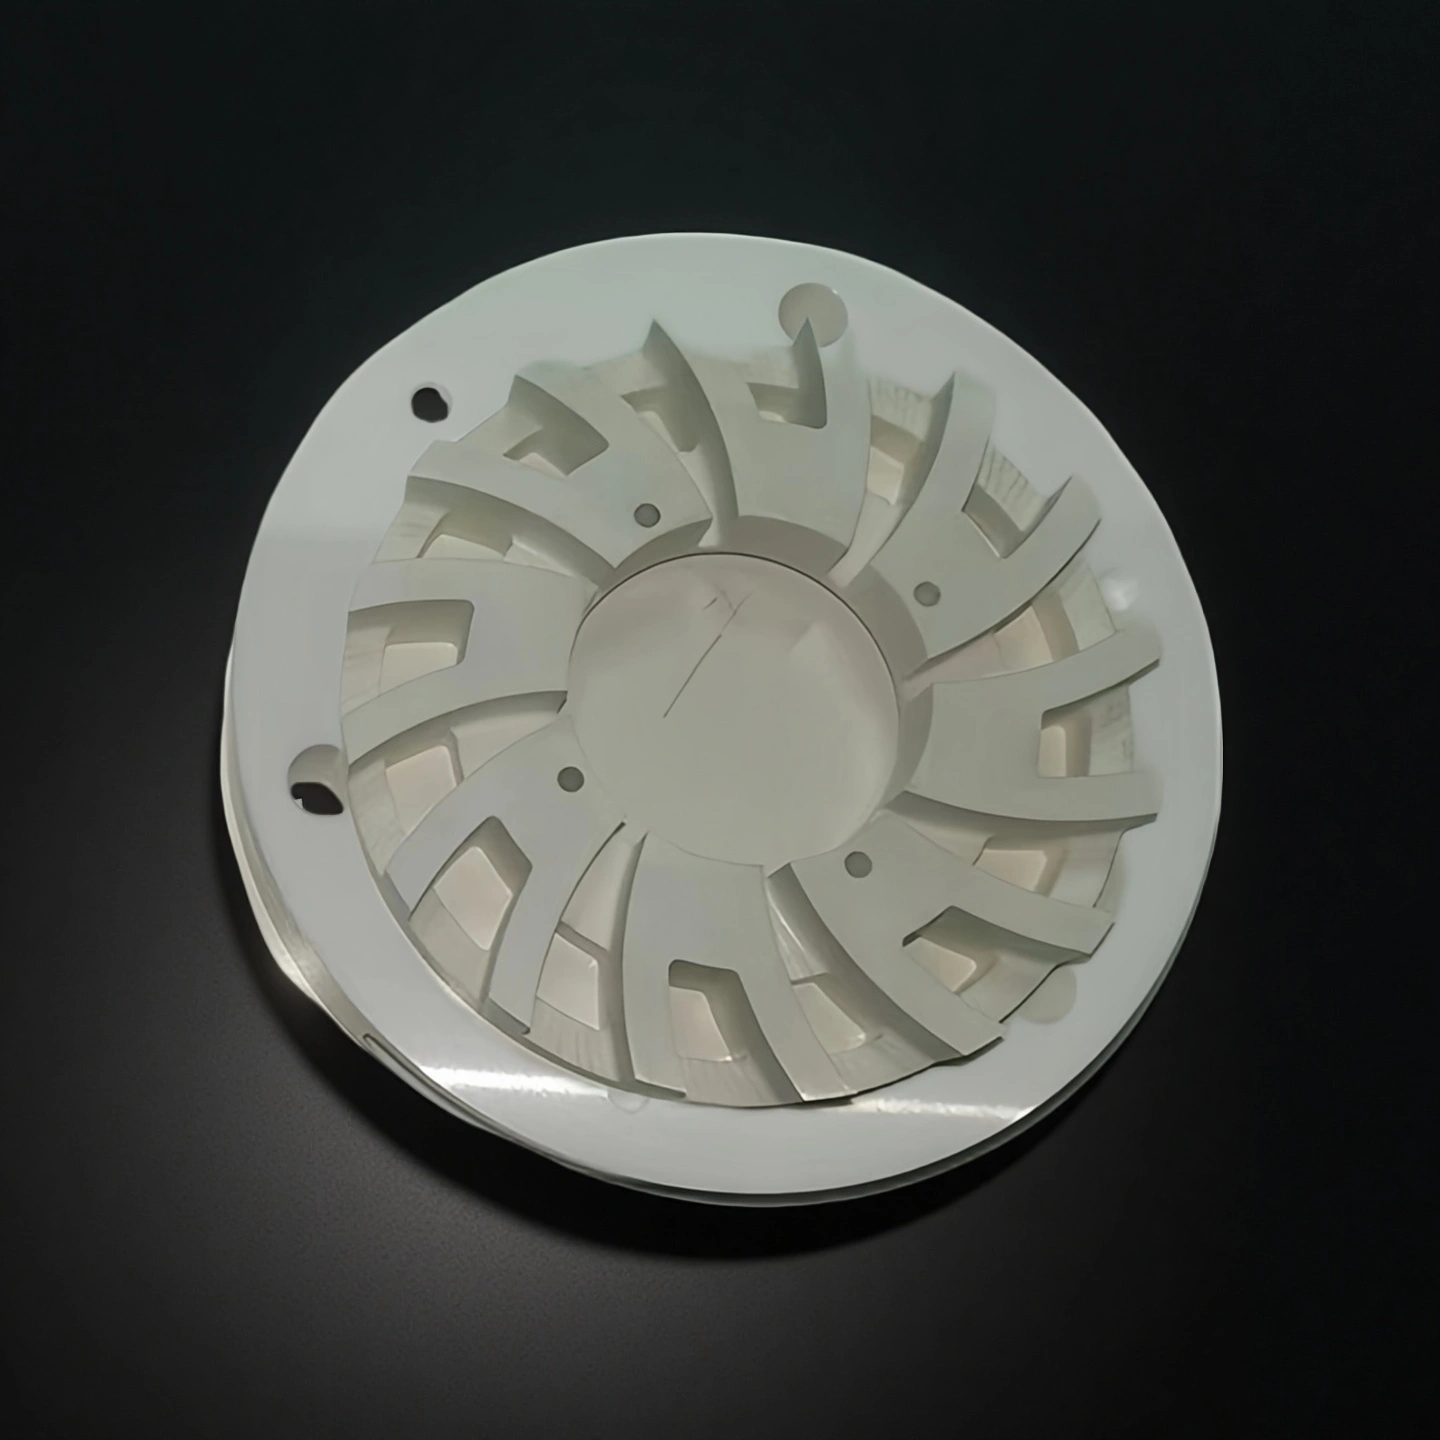
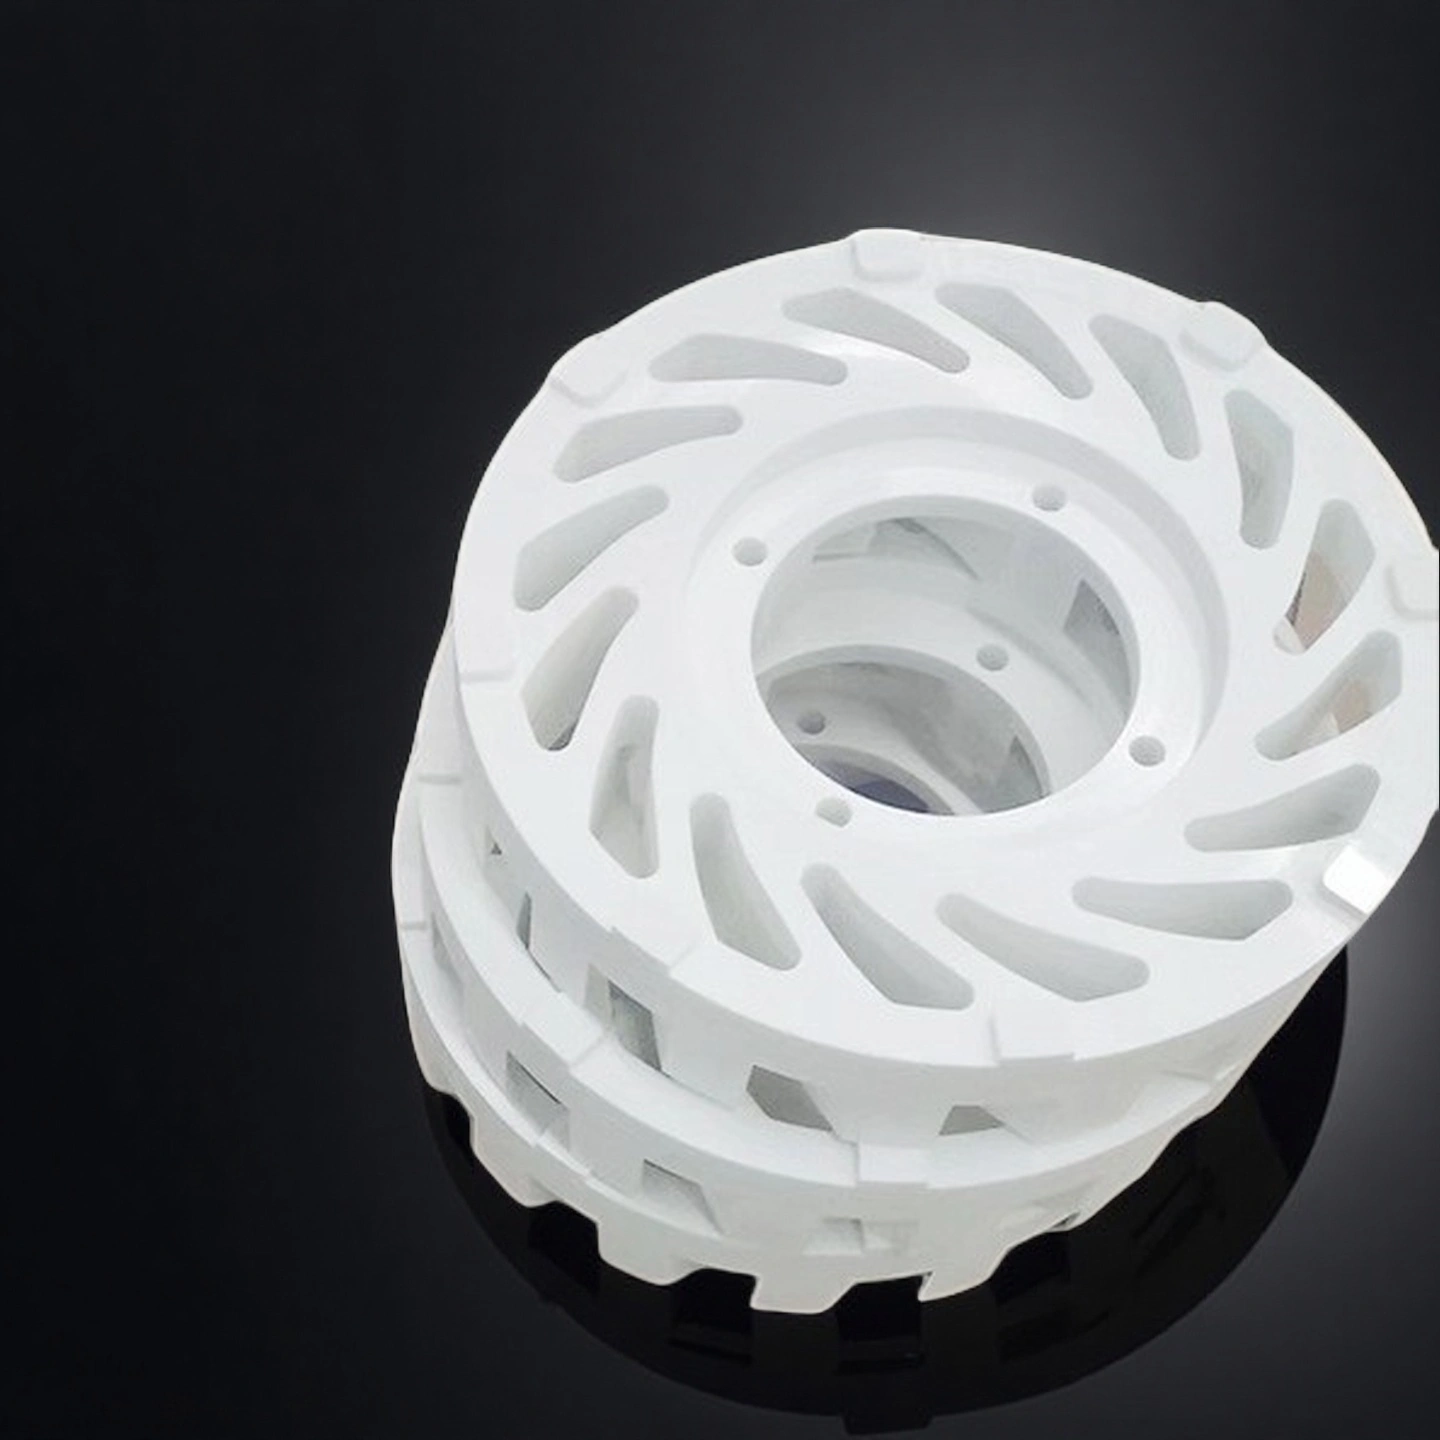
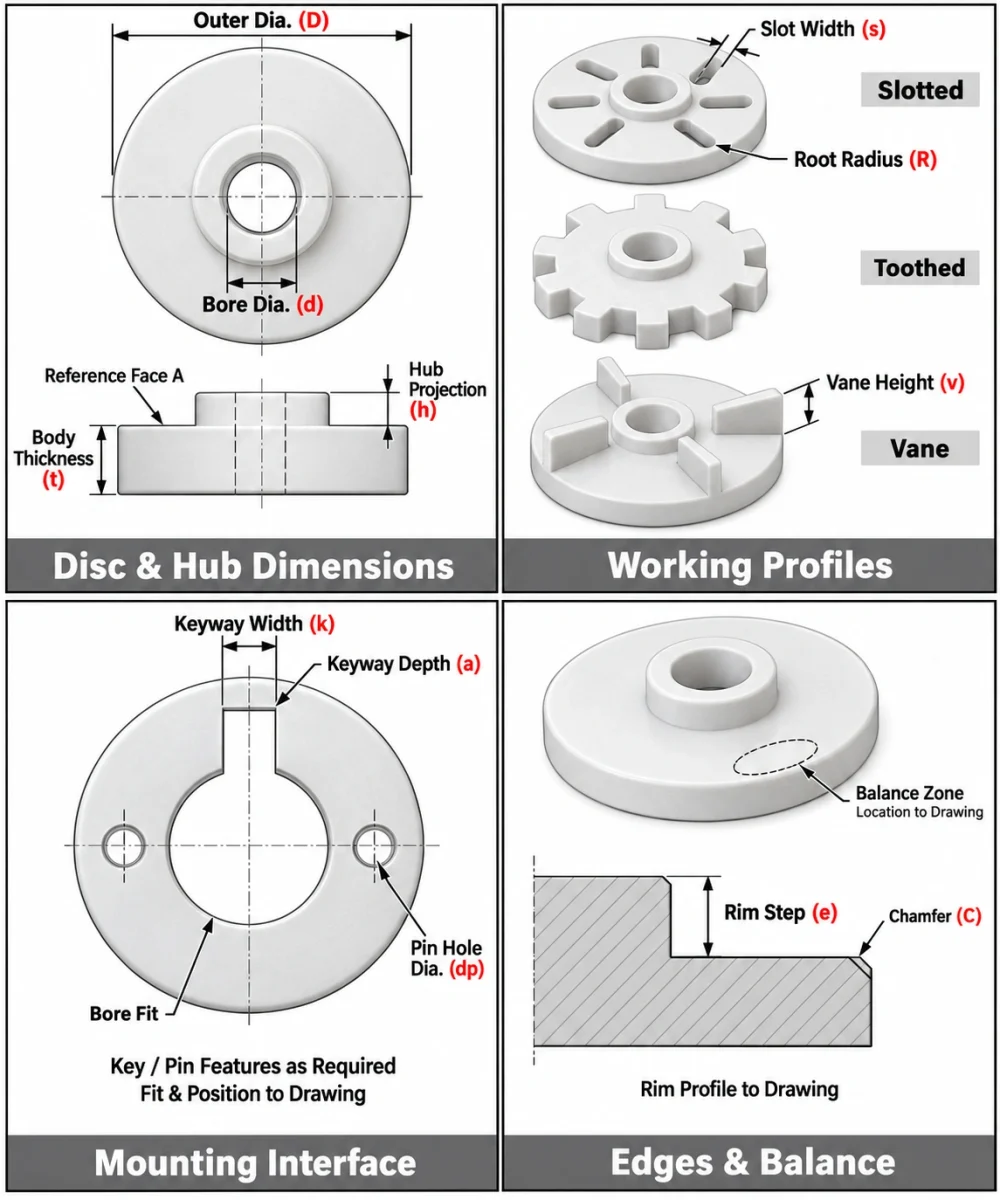
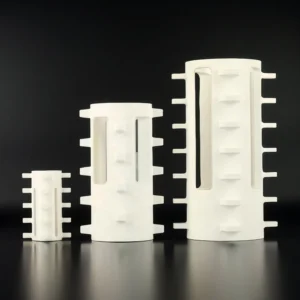
Zirconia ceramic dispersion discs are the rotating wear parts mounted on the shaft of a bead or sand mill. As the shaft turns, the disc drives the grinding beads through the slurry, breaking down pigment and particle agglomerates and keeping the mix moving through the milling chamber. Because the disc controls how the beads move through its section of the chamber, its outer profile, slot or tooth pattern and bore fit matter as much as the material.
ADCERAX supplies the disc to drawing or to the published AT-YHG-SM references, in 3Y-TZP, Mg-PSZ or Ca-PSZ zirconia. Send the disc number or a worn-part sample with the shaft interface; the geometry is reviewed with you and quoted against the drawing and inspection plan.
Specifications of Zirconia Ceramic Dispersion Disc
|
Sand Mill Zirconia Ceramic Disc |
|
Item No. |
Outer Diameter (mm) |
Inner Diameter (mm) |
Height (mm) |
|
AT-YHG-SM001 |
90 |
30 |
26 |
|
AT-YHG-SM002 |
96 |
36 |
24 |
|
AT-YHG-SM003 |
100 |
45 |
30 |
|
AT-YHG-SM004 |
140 |
80 |
45 |
|
AT-YHG-SM005 |
165 |
85 |
50 |
↓Download the Product Catalogue
Zirconia Disc Performance in Bead and Sand Mills
A zirconia dispersion disc must maintain its working profile, shaft fit and position in the stack. Select the material together with the bead impact, mounting loads and slurry conditions.
Four Areas to Review
- Edges and slots: Repeated bead impact can round edges and widen slots. Select for both hardness and fracture toughness.
- Hub and disc body: Torque, startup shock and jams place stress on the hub and web. Compare flexural strength alongside the disc geometry and support arrangement.
- Bore and mounting faces: Define the bore, keyway or pin fit and face tolerances so the disc seats correctly. Check these features against the actual thermal and loading conditions.
- Slurry-contact surfaces: Review the solvent, pH and solids against the selected grade. Chemical suitability must be confirmed for the actual formulation.
Material Comparison
| Material route |
Selection focus |
Typical density (g/cm³) |
Typical flexural strength at 20°C (MPa) |
| AD-ZRO-3Y · 3Y-TZP |
Starting point for structural and wear-contact discs |
6.00–6.08 |
800–1000 |
| AD-ZRO-MG · Mg-PSZ |
Partially stabilized option for project-specific review |
5.70–5.80 |
500–755 |
| AD-ZRO-CA · Ca-PSZ |
Calcium-stabilized option matched to geometry and duty |
5.60–5.75 |
400–600 |
These are typical material-specimen values, not finished-disc speed, torque or service-life ratings. Compare the same properties under matching test conditions. Finished discs are accepted against the drawing and agreed inspection plan.
Choosing the Material
- 3Y-TZP: The usual starting point for discs carrying bead impact and bending loads. It has the highest typical density and flexural strength of the three grades listed.
- Mg-PSZ: Review when the project calls for a partially stabilized structural zirconia, together with the disc geometry and mounting arrangement.
- Ca-PSZ: Consider when the drawing and operating conditions suit a calcium-stabilized zirconia body.
Confirm the material, geometry, mounting interface and operating requirements together during drawing review and first-article evaluation.
How the Three Disc Forms Differ
Slotted, toothed and vane discs have different working geometries. Select the form with the mill maker or through trials using the intended beads, slurry and operating speed.
1. Slotted Discs
- Design: Openings pass through the disc body, allowing slurry to move between its two sides.
- Key dimensions: Slot count, width and root radius.
- Selection focus: Open area and resistance to slurry flow through the disc.
The bore, hub and key or pin features remain defined by the mounting drawing.
2. Toothed Discs
- Design: Teeth around the outer rim create a series of working edges.
- Key dimensions: Tooth count, depth and pitch.
- Selection focus: Interaction between the rim and the grinding beads.
This form suits processes designed around the action of the toothed rim.
3. Vane Discs
- Design: Raised blades on the disc face help move slurry and promote circulation.
- Key dimensions: Vane height, angle and count.
- Selection focus: Slurry circulation within the grinding chamber.
This form suits designs that rely on the disc’s pumping action.
For your enquiry: Send a drawing or clear photo showing the feature count, main dimensions and mounting details. Specify the disc by its geometry, rather than by the form name alone.
Packaging of Zirconia Ceramic Dispersion Disc
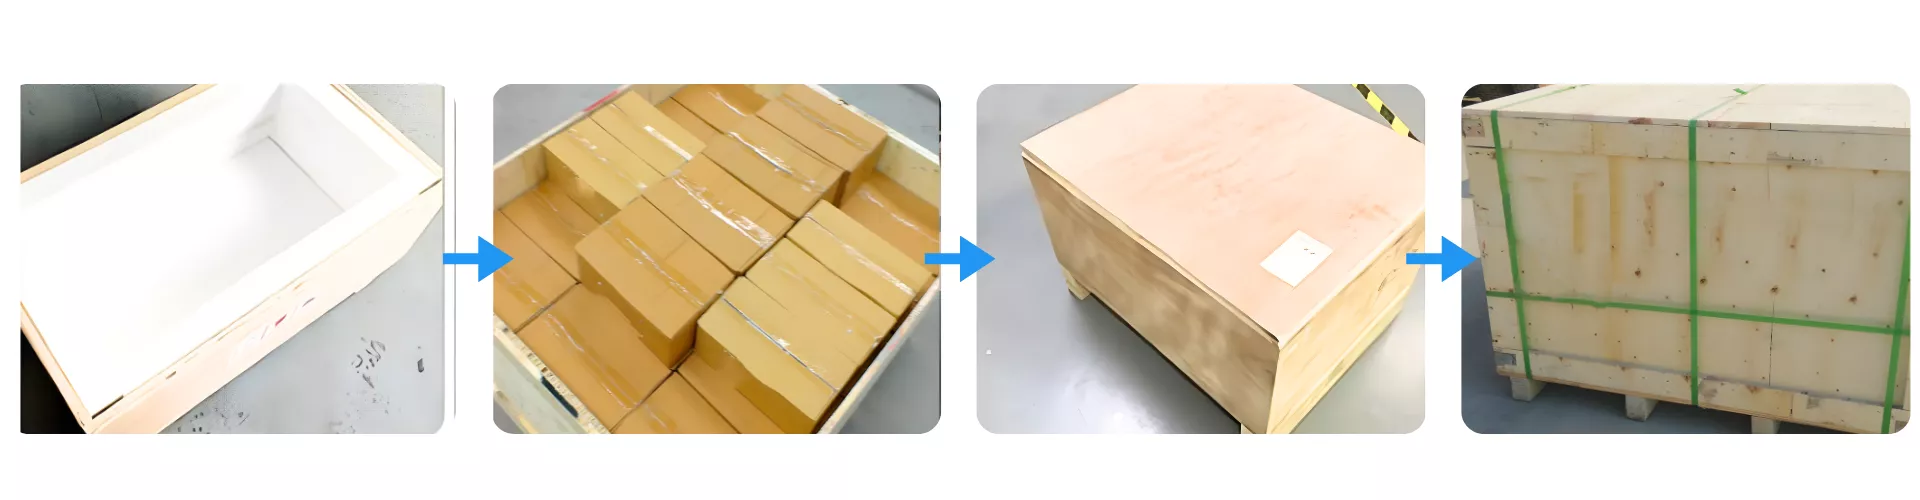
Zirconia Ceramic Dispersion Disc is securely packed using multi-layer protection to prevent mechanical damage during global transit. Each unit is first boxed, then reinforced inside foam-lined wooden crates for shock absorption. Final crates are sealed and strapped to ensure stability during containerized shipping.
Zirconia Dispersion Disc Applications by Milling Duty
The disc is chosen from the duty it runs in. The slurry, the bead charge and the machine set what the disc has to survive, and four project types come up most often in quotation review.
-
Zirconia Dispersion Discs for Coatings and Pigment Dispersions
Coating work runs pigments that must be broken down to a repeatable fineness, and many lines change color between batches. The disc decision here turns on slot and profile geometry and on the contact materials in the wetted path, because both affect how cleanly the line changes over and how much material the disc holds back.
On the drawing, state the working profile and the surfaces that contact the product. For the project, define the slurry chemistry, the bead grade and size, the cleaning method used between colors, and any color or metal-content limit the formulation has to meet, with the sampling plan that checks it. White and light metallic basecoats are the usual reason a metal limit appears in the specification at all.
-
Zirconia Discs for Ink and Fine-Particle Milling
Ink and fine-particle work is judged on particle distribution and on how little material stays in the mill between runs. The disc decision shifts to bore and stack fit, disc spacing and the finish on the wetted faces, since these set how the disc sits in the group and how readily the surfaces release product.
Define the viscosity range the mill runs, the target particle distribution and the method used to measure it, the residue check after cleaning, and the fit criteria for the disc on the shaft. Where a change in distribution is traced to the disc, the group spacing and the fitted position are the first things to confirm.
-
Dispersion Discs for Battery and Electronic Slurries
Battery and electronic slurries add a contamination question to the wear question. The disc decision covers the whole contact chain in the chamber: disc, bead, liner and shaft sleeve, because a part that sheds or reacts anywhere in that chain reaches the slurry the same way.
On the drawing, state the selected zirconia route and the wetted surfaces. For the project, name the solvent, the solids loading and the temperature, the specific elements the formulation limits, and the acceptance method used to check them. Naming the elements and the method is what turns a contamination requirement into something a supplier can inspect against.
-
Replacement Zirconia Discs for Mill OEMs and Second-Source Supply
OEM and second-source projects start from an existing disc rather than from a blank sheet. The decision here is about identity: which OEM disc the part replaces, how it interfaces with the shaft, where it sits in the disc group, and what the group geometry around it looks like.
Provide the machine model and serial where available, the old part drawing or a sample, and the speed and torque the mill applies. Agree the runout criteria for the assembly before the first part is made, so the replacement is judged the same way the original was. Second-source supply is quoted against the same drawing the OEM part was made to, with any deviation stated rather than left to assumption.
Safe and Efficient Use of Zirconia Ceramic Dispersion Disc
A zirconia dispersion disc is a hard, brittle wear part. It carries load well inside the mill and far less well outside it, so most avoidable damage happens at unpacking, at the shaft or during a clean.
-
Handling and Storage Recommendations
1. Avoid Mechanical Shock
Move the disc in padded carriers, and never let two discs strike edge to edge. A chip or micro-crack starts there and fails later in service.
2. Keep in Dry Conditions
Store dry and away from condensation. Damp packing leaves residue on the bore and working faces.
3. Wear Clean Gloves
Handle with clean nitrile gloves. Oil and skin residue on a working face end up in the slurry.
4. Rest It Correctly
Never stand the disc on its working face on a bare bench. Use a soft, clean surface or leave it in its packing.
-
Installation in the Mill
1. Check Spindle Alignment
Verify concentricity with a dial gauge to the equipment manual. An eccentric spindle wears the rim unevenly.
2. Confirm a Secure Mount
Clean the shaft, hub face and keyway or pin of burrs, then tighten to the manual's torque. A loose bore slips under load.
3. Clean the Interfaces
Wipe the mounting contacts with lint-free cloths. A trapped chip reads as runout and as vibration.
4. Confirm the Stack Order
Check order, spacing and fitted position against the drawing before the stack is closed.
-
Startup and Operation
1. Never Start Dry
Confirm the fluid volume and the liquid conditions specified for the mill. A dry or partly filled chamber is the usual first-run failure.
2. Watch Vibration, Noise and Temperature
Compare the first batches with the mill's earlier baseline. Rising vibration or new resonance points to worn geometry or a mounting error.
3. Stop and Inspect
If a reading is unusual, stop per the equipment procedure and inspect before restarting. A changed profile does not correct itself.
4. Follow the Approved Cycle
Run the cycle approved for the equipment, the slurry and the grade. Any pause comes from the manual, not from the disc.
-
Cleaning and Batch Records
1. Clean Non-Abrasively
Use the method approved for the grade and the slurry. Hard brushes and aggressive chemistry open micro-scratches that hold product.
2. Inspect After Each Batch
Check the bore, slots or teeth, rim and functional faces at each clean. Record uneven polish loss, edge rounding, slot growth or pitting.
3. Log Time, Speed and Wear
Keep batch time, speed and a short note or photo at each service. Replace on that evidence, not on a calendar interval.