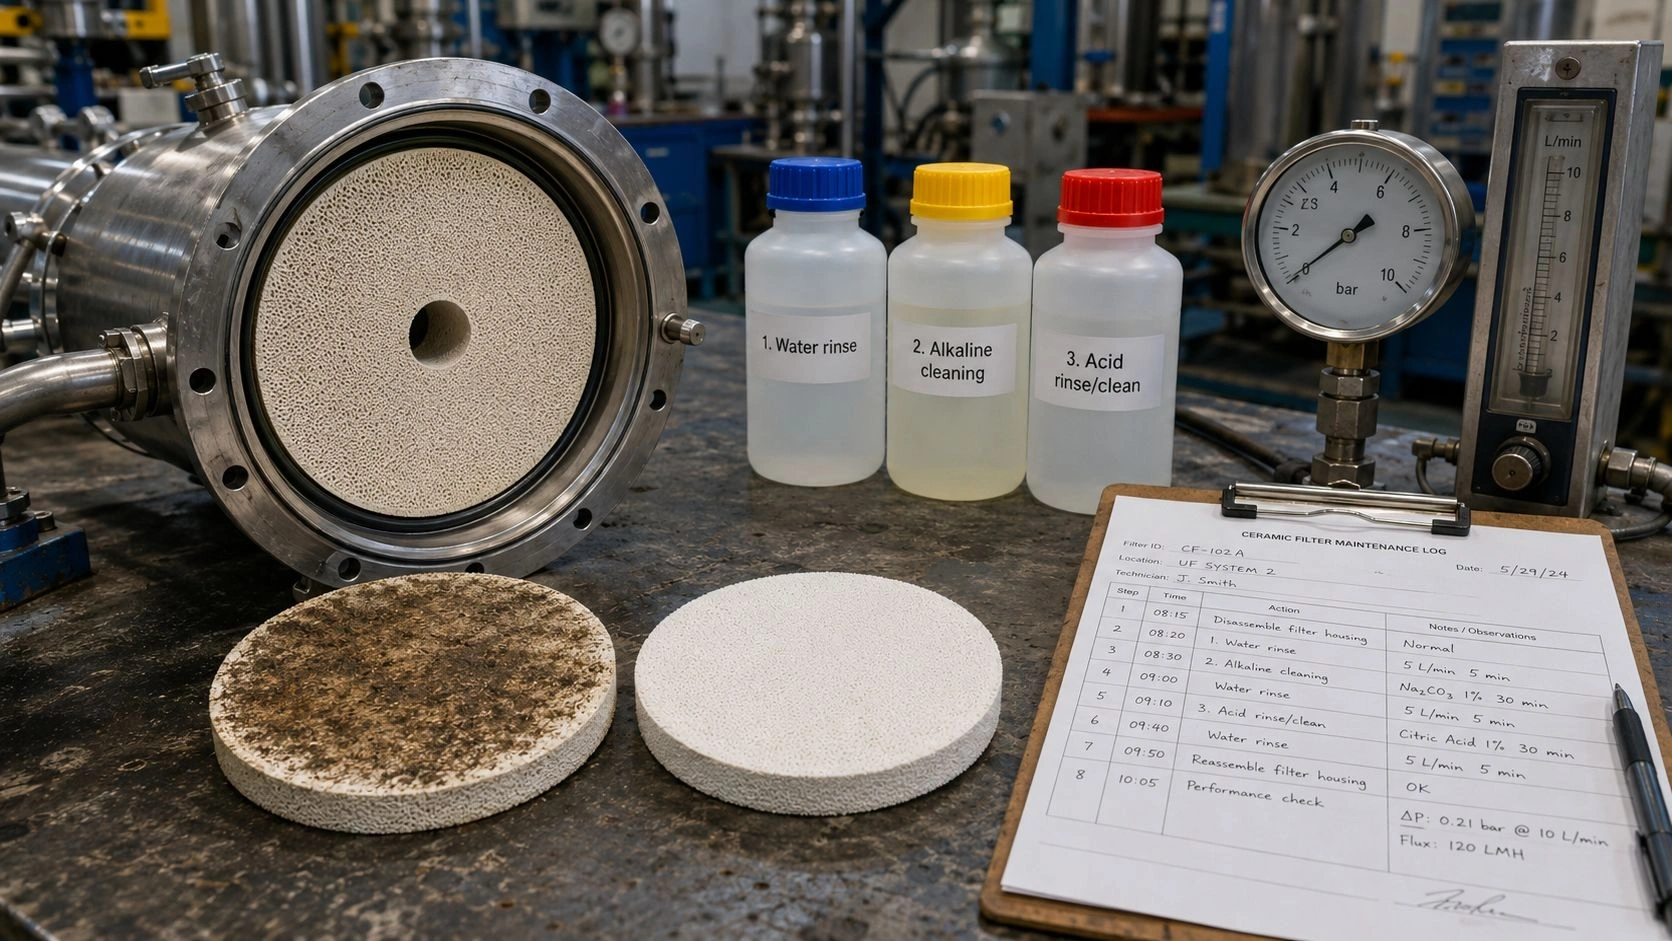
Microporous alumina filter tubes are engineered ceramic components with precise pore architectures that enable selective separation across gas and liquid phases. Their utility spans from demulsification in petrochemical plants to catalytic support in hydrogen systems. These tubes combine thermal durability, chemical inertness, and customizable porosity to meet the challenges of high-demand filtration tasks.
Unlike polymeric or metallic filters, alumina-based solutions maintain performance in extreme temperatures and chemically aggressive media. Catalog-typical pore windows often fall between 0.1–10 µm as RFQ screening ranges — confirm on drawing + duty. This adaptability supports both catalog geometries and drawing-based industrial systems.
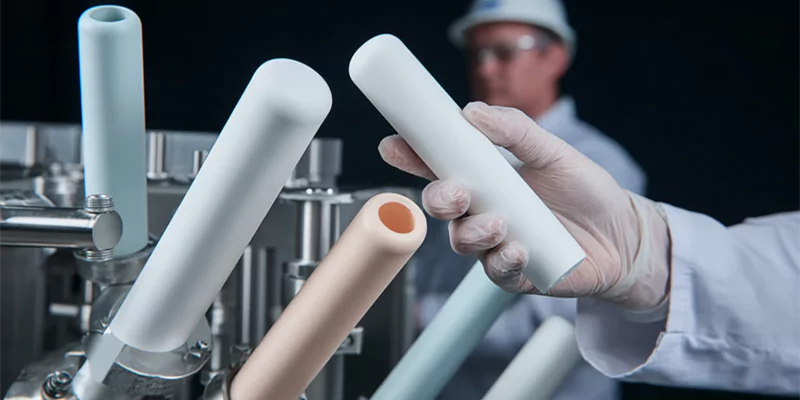
This article walks microporous alumina filter tubes from material fundamentals through manufacturing, structural parameters, applications, case screening language, limitations, and RFQ fields. Use it to lock pore size, porosity, wall thickness, ΔP, media, and duty — not as a factory SLA. Product context: microporous alumina filter tube; family: alumina tubes; drawing-based RFQ: custom ceramic services.
I. Fundamentals of Microporous Alumina Filter Tubes
Microporous alumina filter tubes are ceramic components designed with interconnected pores, enabling selective separation of fluids and particles. Their structural design directly affects performance in demanding filtration and demulsification applications. Understanding their core materials, pore characteristics, and mechanical behavior forms the basis for effective deployment in industrial systems.
Definition and Core Material Composition
Microporous alumina tubes are typically fabricated from alpha-phase aluminum oxide (Al₂O₃), a high-purity ceramic known for exceptional thermal and chemical stability. The material composition determines the tube’s inertness to acids and bases, and its sintered grain structure supports long-term structural integrity. Alumina’s stable crystalline configuration makes it ideal for both gas and liquid filtration under harsh environments.
The ceramic body is usually processed through sol-gel or extrusion methods to achieve the desired tube form before pore structure is introduced. High-purity raw powders (>99.5% Al₂O₃) are used, minimizing impurities that could weaken the mechanical structure or leach into the filtered media. Post-forming calcination at temperatures around 1600 °C locks the microstructure into place.
This ceramic chemistry serves as a foundation for performance consistency, especially when filtration conditions demand thermal resistance above 1000 °C and exposure to reactive compounds.
Pore Formation Mechanisms and Structural Features
Pore formation is primarily achieved through sacrificial templating1 or gas-releasing agents during sintering. These controlled processes result in a network of interconnected micropores2, typically ranging from 0.1–10 µm as catalog-typical RFQ screening windows — confirm on drawing + duty. Such porosity directly influences permeability and selectivity across fluid systems.
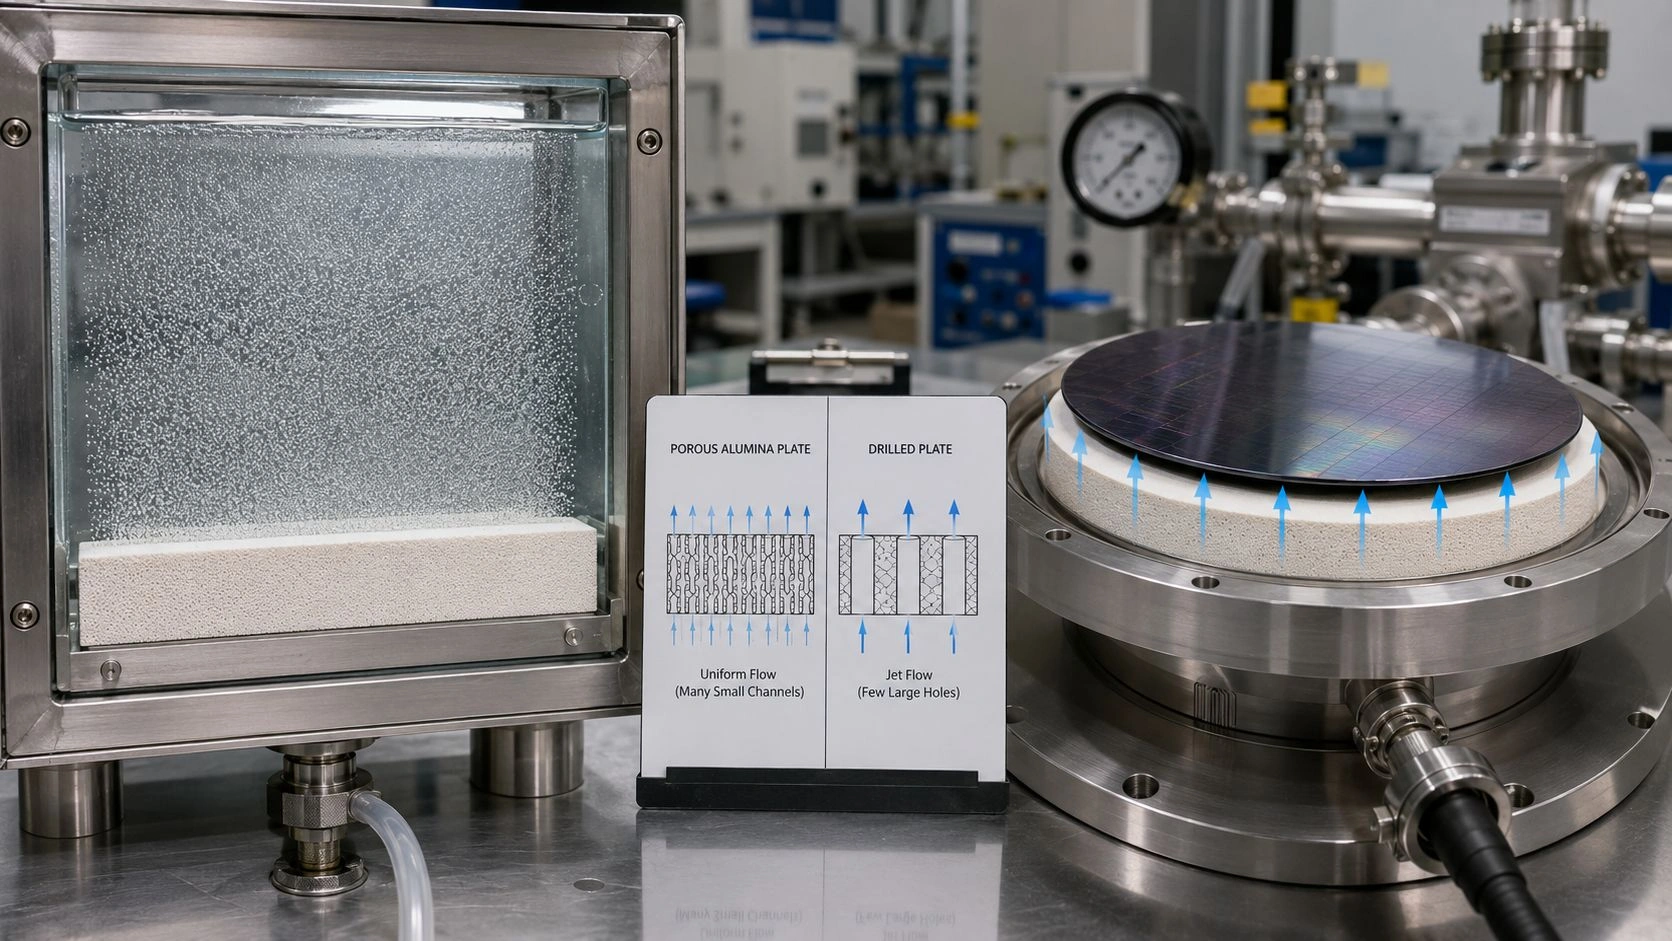
The interconnectivity of pores determines pressure drop and flow uniformity, both critical to applications like oil-water demulsification or catalyst support. Pore shapes and throat dimensions are also optimized for mechanical strength, ensuring filtration does not collapse under operational pressure. In high-end applications, engineered gradients in pore density are applied along the tube wall to control separation layers.
To summarize key design priorities in micropore structuring:
- Pore Diameter Control: Maintains flow balance and particle capture.
- Interconnected Geometry: Ensures low pressure drop and high flux.
- Sintering Uniformity: Prevents structural failure under stress.
Key Performance Metrics: Porosity, Permeability, and Durability
The porosity of microporous alumina tubes is often cited in a 25–45% screening band, balancing mechanical strength and permeability — confirm on grade sheet + drawing + duty. Higher porosity enables faster filtration rates but may compromise structural stiffness. Engineers must balance these metrics according to application needs.
Permeability values are commonly quantified using Darcy’s Law, with industrial tubes offering flux rates up to 2000 L/m²·h·bar. Durability is assessed through cyclic pressure testing. Cycle counts and differential pressure (often discussed around multi-bar duty) are pressure-/cycle-dependent — confirm on drawing + duty; not a factory acceptance SLA.
| Metric | Typical Range | Importance |
|---|---|---|
| Porosity | 25–45% screening — confirm on drawing + duty | Controls filtration speed & strength |
| Permeability | >1000 L/m²·h·bar | Indicates flow capacity |
| Cyclic Strength | Pressure-/cycle-dependent — confirm on drawing + duty | Lifespan screening (not acceptance SLA) |
II. Manufacturing Processes and Quality Control
Reliable performance of microporous alumina filter tubes depends on stable and repeatable manufacturing processes. From raw material selection to thermal sintering, each step directly affects pore uniformity and structural strength. This section details key process techniques, additive strategies, and quality testing frameworks adopted by industrial suppliers.
Extrusion and Thermal Sintering Techniques
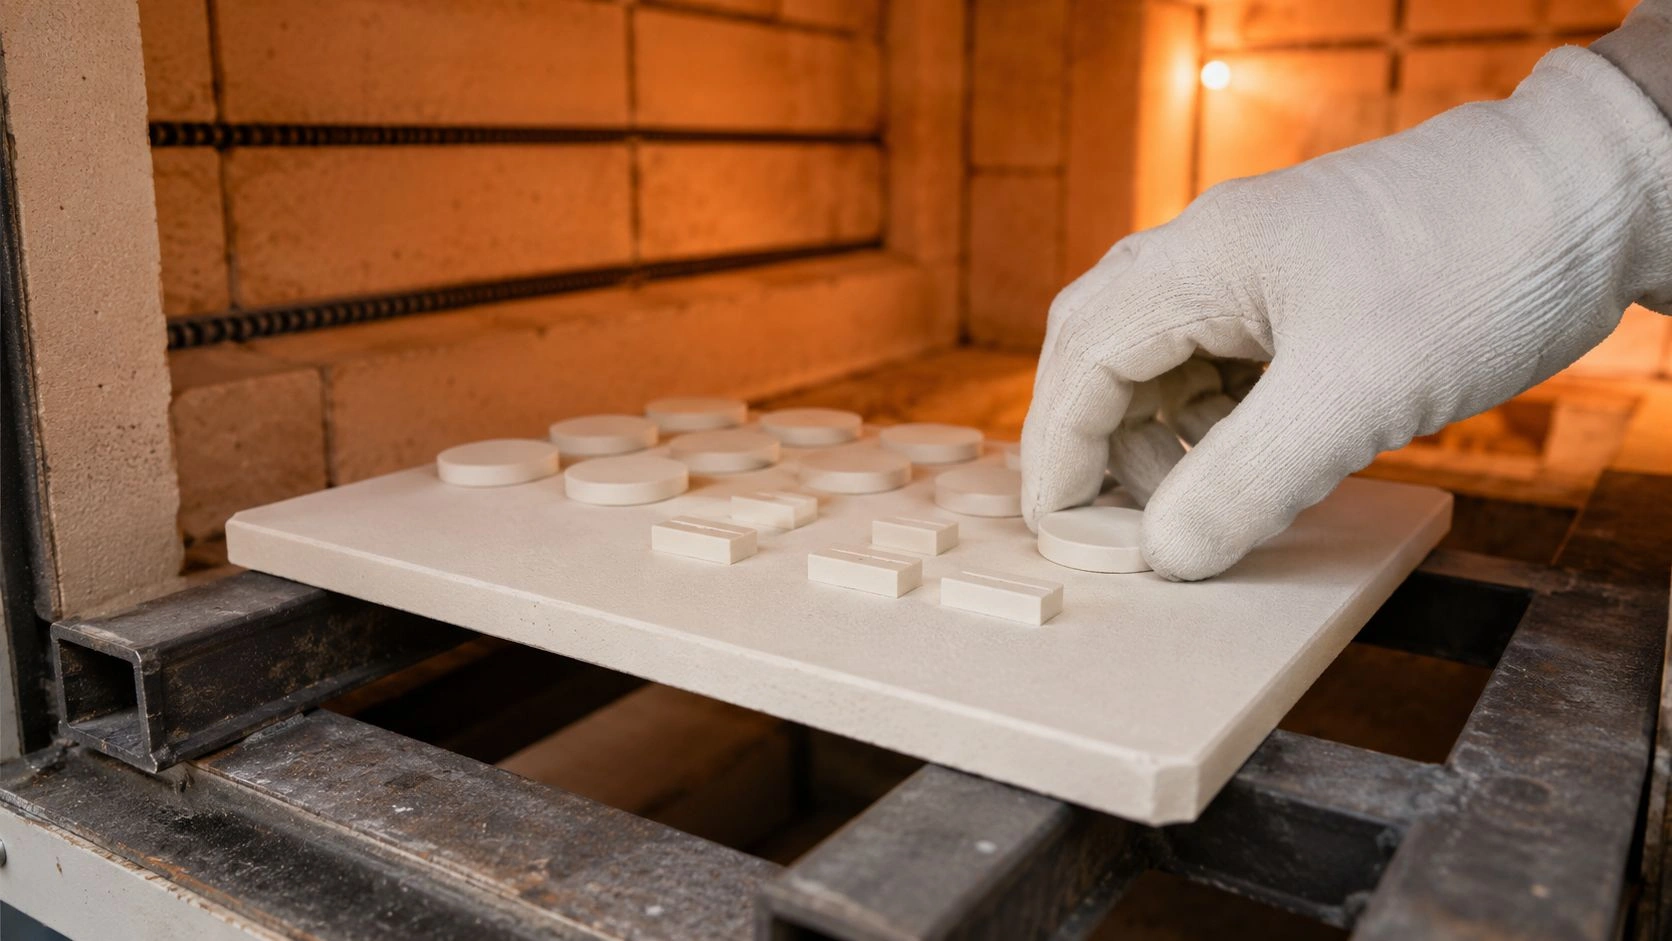
Extrusion is the dominant forming method for filter tubes due to its ability to produce consistent internal channels and external dimensions. Alumina powder mixed with binders and plasticizers is extruded into cylindrical tubes with controlled wall thickness. After drying, green bodies retain form but require thermal treatment to achieve ceramic strength.
The sintering process is typically conducted between 1400–1650 °C depending on the target density and pore design. During this high-temperature firing, organic additives are burned off and alumina grains fuse together, locking in porosity and mechanical strength. The sintering profile—heating rate, dwell time, and cooling—is tightly controlled to avoid warping or microcracking.
To highlight essential extrusion-sintering relationships:
- Binder Removal Profile: Influences pore size retention.
- Sintering Temperature Window: Determines final density and strength.
- Cooling Curve Management: Prevents residual stresses in tube walls.
Role of Additives and Grain Size Control
Additives play a critical role in tailoring pore structure and mechanical resilience. Organic pore formers, such as starch or polymethyl methacrylate (PMMA), decompose during sintering to leave behind voids that become functional micropores. The type and volume fraction of these agents define pore diameter distribution and connectivity.
Grain size control of the base alumina powder is equally vital. Finer grains (<1 µm) promote uniform densification and reduce crack propagation, whereas coarser grains (>3 µm) may improve thermal shock resistance but compromise filter finesse. Optimal blends are often used to balance permeability with mechanical robustness.
Pore control strategies depend on:
- Template Chemistry: Shapes final pore geometry and stability.
- Grain Fineness: Enhances sintering homogeneity and reduces defects.
- Additive Ratios: Balance porosity and strength per application demand.
Industry Standards and ISO/ASTM Testing Frameworks
To ensure global compatibility and quality assurance, alumina filter tubes are manufactured and tested according to international standards. ISO 2768 governs general tolerances in ceramic extrusion, while ASTM F795 outlines porosity, permeability, and mechanical strength testing for porous ceramics.
Standard tests include bubble point pressure testing3 to verify pore continuity, flexural and compressive strength testing for structural validation, and chemical stability tests4 under acidic and basic environments. Suppliers with ISO 9001 certification typically integrate these methods into their production SOPs.
| Test Method | Standard | Function |
|---|---|---|
| Bubble Point Test | ASTM F316 | Evaluates pore opening continuity |
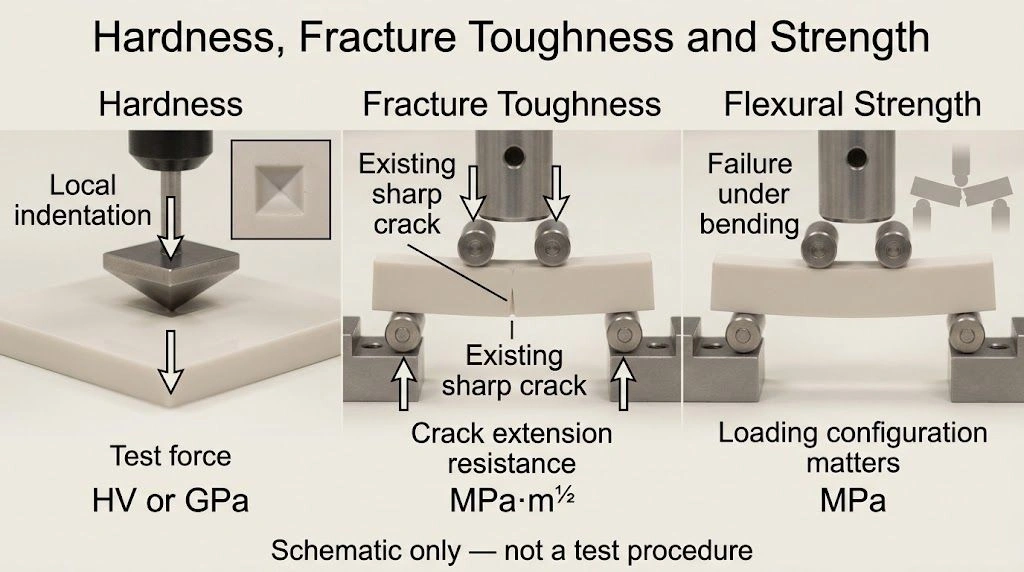
| Flexural Strength | ISO 14704 | Assesses mechanical resistance |
| Chemical Soak Test | ASTM C650 | Verifies acid/base stability |
III. Structural Properties Driving Filtration Performance
The performance of microporous alumina filter tubes is closely tied to their structural configuration. Attributes such as pore size, wall thickness, and thermal resistance determine how effectively these tubes function in filtration-intensive environments. This section examines how each parameter contributes to fluid dynamics, mechanical reliability, and chemical durability.
Influence of Pore Size Distribution on Efficiency
Pore size plays a pivotal role in separation efficiency. Microporous alumina tubes typically feature pores ranging from 0.1–5 µm as catalog-typical RFQ screening — confirm on drawing + duty — enabling filtration of emulsions and fine particulates when matched to feed. Uniform distribution minimizes flow dead zones and ensures consistent pressure drop across the filter.
Finer pore control (often discussed below ~1.5 µm for oil-water demulsification) can improve rejection when matched to droplet size — confirm on duty RFQ; not a removal-rate SLA. Broader distributions lead to uneven flow, clogging, or incomplete separation. Therefore, manufacturers apply pore size classification using mercury porosimetry or gas flow techniques to maintain consistency.
Several principles govern this structure-performance relationship:
- Tighter Pore Range: Improves rejection rates of submicron particles.
- Pore Uniformity: Reduces flow resistance and clogging risk.
- Size-to-Pressure Ratio: Balances throughput with selectivity.
Effects of Tube Thickness on Flow and Strength
Tube wall thickness affects both mechanical durability and hydraulic performance. Thicker walls provide greater crush resistance and longer service life under cyclic loading. However, excessive thickness can hinder flow rates and raise operating pressure requirements.
For industrial demulsification systems, a 3–6 mm wall thickness range is typical. Wall thickness trades flow against crush resistance in a duty-/feed-dependent way — confirm on drawing + duty; not a factory flow SLA. Engineers must balance strength and hydraulic performance during design.
To illustrate trade-offs related to thickness:
| Wall Thickness (mm) | Flow impact (screening) | Mechanical impact (screening) |
|---|---|---|
| 2.5 mm | Lower ΔP / flow penalty — confirm on duty | Moderate crush margin — confirm on drawing |
| 5.0 mm | Medium ΔP / flow trade-off — confirm on duty | Higher crush margin — confirm on drawing |
| 7.0 mm | Higher ΔP / flow penalty — confirm on duty | Highest crush margin in this set — confirm on drawing |
Thermal and Chemical Resistance Under Harsh Conditions
Microporous alumina exhibits excellent resistance to extreme temperatures and aggressive chemicals. Melting point is often cited above 2000 °C as teaching context only. Thermal conductivity for dense alumina TDS grades is sometimes near ~25 W/m·K — do not treat that as porous filter-body k; confirm k on porous-body data / duty. Microporous tubes remain useful under high-heat filtration when matched to oxidizing duty. This makes it suitable for catalytic filtering or exhaust gas treatment.
Chemically, α-Al₂O₃ is inert to most acids and bases, except under hydrofluoric acid or strong alkali fusion. Long-term soak behavior is media-dependent — confirm soak protocol on duty RFQ (not a mass-loss % SLA). Its resistance extends to oxidizing agents and chlorinated solvents, making it ideal for chemical refineries.
Important thresholds for thermal-chemical endurance include:
- Max Continuous Temp: ~1200 °C oxidizing screening — confirm on grade sheet + duty.
- pH Compatibility: pH 2–11 screening band — confirm soak protocol on duty RFQ.
- Corrosion Rate: Media-dependent — confirm soak protocol on duty RFQ.
IV. Industrial Applications Across Engineering Sectors
Microporous alumina filter tubes serve as core components across multiple engineering sectors requiring reliable solid-liquid or gas-solid separation. Their unique combination of pore control, chemical resistance, and structural integrity makes them especially suitable for demanding environments. This section presents key application areas, each driven by specific performance criteria.
Oil-Water Separation and Demulsification Efficiency
In oil refining and wastewater management, alumina tubes are widely used for phase separation. Their microporous architecture promotes capillary-driven phase inversion, allowing rapid separation of stable emulsions. Demulsification performance is sector-typical / feed-dependent when pore size is matched to droplet size (often discussed below ~1.2 µm) — confirm on process data; not a removal-rate SLA.
Throughput and energy outcomes are duty-/feed-dependent screening results — not factory SLA. Attribute gains to coalescence time and flux uniformity only after confirming on the ordered duty RFQ.
Critical mechanisms enhancing demulsification include:
- Capillary Pinning Effect: Promotes water retention while repelling oil.
- Pore-Induced Pressure Gradient: Accelerates interface displacement.
- Surface Wettability: Alumina’s hydrophilic nature aids water permeation.
Gas Purification in Petrochemical and Chemical Plants
Alumina filter tubes are essential in gas-phase processes for removing aerosols, fine particles, or catalyst residues. Their high thermal tolerance makes them suitable for post-combustion scrubbing, ammonia purification, and VOC removal from flue gas.
Finer pores (e.g. ~0.3 µm screening) can cut carryover when matched to feed — confirm on duty RFQ; not a contamination-% SLA. High-temperature hold time (sometimes discussed near hundreds-to-thousands of hours around ~400 °C) is duty-dependent — confirm on drawing + duty; do not treat page hours as a contract life line.
Performance gains in gas treatment include:
| Application Type | Screening language | Operating Temp (screening) |
|---|---|---|
| VOC Scrubbing | Sector-typical screening — confirm on process data | <300 °C screening |
| HCl Removal | Sector-typical screening — confirm on process data | 250–350 °C screening |
| Aerosol Filtration | Sector-typical screening — confirm on process data | <450 °C screening |
Catalytic Supports and Hydrogen-Related Processes
Microporous alumina is used as a carrier for catalysts in hydrogenation and steam reforming due to its high surface area and thermal stability. The porous tube provides a stable scaffold that resists collapse or sintering under cyclic thermal loads.
Catalyst activity and sulfur-poisoning resistance are duty-/feed-dependent screening comparisons versus granular substrates — confirm on process data / procurement RFQ. Cycle length between regenerations is not a factory life SLA.
These benefits are primarily enabled by:
- High Surface Area: Enhances active site dispersion.
- Dimensional Rigidity: Prevents structural collapse under gas flow.
- Inert Chemical Profile: Minimizes side reactions or contamination.
V. Case Studies and Comparative Insights
Case studies provide engineering teams with grounded performance data to evaluate material suitability in industrial-scale scenarios. By analyzing field-tested results from real-world installations, users can assess how microporous alumina filter tubes compare with traditional or alternative solutions. This section consolidates performance outcomes and material comparisons in demanding filtration environments.
Performance in Oil Refinery Operations
In a 2023 field trial at a coastal oil refinery in Canada, microporous alumina tubes were installed to replace PTFE membrane systems in the demulsification unit. Over a multi-week trial window, alumina tubes showed duty-/feed-dependent throughput and oil-rejection screening behavior under variable feed — confirm on process data; not factory KPI SLA.
The improvement was largely attributed to the superior wetting dynamics and reduced fouling rates. Operators noted that cleaning frequency was reduced from once every 36 hours to once every 72 hours, resulting in significant labor and downtime savings.
The following observations summarize their performance advantages:
- Reduced Fouling Rate: Cleaning interval can lengthen when matched to feed — confirm on duty RFQ.
- Higher Permeate Flow: Throughput is duty-/feed-dependent screening — not factory SLA.
- Operational Stability: Multi-bar duty is pressure-/cycle-dependent — confirm on drawing + duty.
Applications in Environmental Engineering Projects
Environmental engineering projects, especially in water remediation and air quality control, benefit from the chemical inertness and long life of alumina tubes. In a municipal wastewater plant in Poland, microporous alumina elements were used to filter heavy metal ions and organic pollutants.
During multi-month operation, heavy-metal and VOC removal were sector-typical / process-dependent screening outcomes — confirm on process data; not removal-% SLA. Versus polymeric membranes, alumina tubes often show better chemical fatigue resistance; CIP cycle counts remain duty-dependent — confirm on drawing + duty.
Benefits highlighted in this application include:
| Performance Metric | Alumina Tubes | Polymeric Membranes |
|---|---|---|
| Heavy Metal Removal | Confirm on process data | Confirm on process data |
| Chemical Resistance | Excellent | Moderate |
| Maintenance Interval | >6 weeks | 2–3 weeks |
Benchmarking Against Zirconia and Silicon Carbide Tubes
Material selection often comes down to trade-offs between cost, thermal resilience, and pore stability. Microporous alumina, zirconia, and silicon carbide (SiC) are top contenders in ceramic filtration applications. Comparative lab tests under simulated harsh conditions provide useful guidance.
Alumina performed best in moderate-temperature scenarios (up to 600 °C), offering a strong cost-performance balance. Zirconia excelled in fracture toughness and SiC demonstrated superior resistance to thermal shock. However, alumina exhibited better pore uniformity and was the most economically scalable.
Key takeaways from material benchmarking include:
- Alumina: Best for general use, low-cost, stable pore structure.
- Zirconia: High strength and toughness; costly.
- SiC: Best for high thermal shock environments; lower pore consistency.
VI. Suitability, Limitations, and Alternative Solutions
Understanding the operational boundaries and limitations of microporous alumina filter tubes is essential for optimizing system design. While they offer high thermal and chemical stability, there are specific scenarios where their use may be constrained. This section also explores alternative materials suitable for these edge cases.
Operational Boundaries: High Acidity, High Pressure, or Cost Constraints
Microporous alumina filter tubes excel in neutral and mildly alkaline environments, but face degradation in extreme acidic conditions. For example, in sulfuric acid environments (pH < 2), alumina may show micro-cracking over time, leading to pore instability and reduced filtration accuracy.
Additionally, systems at elevated multi-bar duty may require structural reinforcements or alternative ceramic compositions — pressure-/cycle-dependent; confirm on drawing + duty (not a hard >12 bar acceptance cutoff on this page). Cost is another limiting factor—alumina tubes, while more affordable than zirconia, are still pricier than polymeric filters for large-scale low-specification needs.
Consider the following contextual limitations:
- Acid Vulnerability: Structural weakening in pH < 2.
- Pressure Limitation: Elevated multi-bar duty — confirm on drawing + duty.
- Cost Barrier: Unsuitable for low-budget, low-risk applications.
Limitations in Scaling and Maintenance Challenges
When filtration systems scale beyond 10,000 L/h, challenges arise in maintaining flow uniformity across multiple alumina tubes. Uneven pore loading or alignment inconsistencies can create pressure gradients, increasing energy consumption and risking membrane fouling.
Moreover, while alumina tubes exhibit excellent fouling resistance, their brittleness requires careful handling during installation and maintenance. Fracture incidents are most common during CIP operations involving sudden temperature changes.
A table of practical constraints in large-scale systems:
| Constraint Type | Impact on Operation | Suggested Mitigation |
|---|---|---|
| Flow Distribution | Uneven pressure zones | Use flow restrictors |
| Handling Fragility | Risk of micro-cracking | Preheat before CIP |
| Scaling Complexity | Complex support structure | Modular frame design |
Alternative Ceramic Options for Specialized Scenarios
In cases where microporous alumina is technically unsuitable, other ceramics offer viable alternatives. Zirconia tubes provide superior mechanical strength and are ideal for corrosive acidic media. Silicon carbide (SiC) options are better for rapid thermal cycling and abrasive flows.
However, these alternatives come with trade-offs. Zirconia is cost-prohibitive in bulk applications, and SiC may have larger pore size variability. Selection must align with both material requirements and process economics.
Scenarios where alternatives are preferred:
- Zirconia: High-strength, acidic media (pH < 2).
- SiC: High thermal shock and abrasive conditions.
- Glass-Ceramics: Optical transparency, lower mechanical load.
VII. Procurement Strategies and Lifecycle Cost Analysis
Procurement for microporous alumina filter tubes should balance upfront cost, duty life, and supply reliability. Lock purity, geometry, and inspection on RFQ — treat page cost deltas as screening, not catalog % SLA.
Cost Drivers: Material Purity, Processing, and Customization
The base cost of microporous alumina filter tubes is highly dependent on material purity levels. For instance, higher-purity (e.g. 99.8%) alumina grades typically cost more than lower-purity (e.g. 95%) grades but can offer better thermal stability and corrosion resistance in high-demand environments — confirm price delta on procurement RFQ; not a catalog % SLA.
Processing methods such as extrusion and precision sintering also influence pricing. Custom geometries (e.g. extended lengths, non-catalog OD/ID) typically raise unit cost on small batches — confirm on procurement RFQ; not a catalog % SLA. (Multi-bore filtration is a different geometry family — keep this page on microporous filter tubes.)
Key cost drivers influencing procurement include:
- Purity Levels: Higher purity = higher cost but better performance.
- Geometry Complexity: Custom shapes increase per-unit price.
- Production Volume: Small batches raise marginal manufacturing cost.
Lifecycle Management and Replacement Cycles
While initial investment may be significant, microporous alumina filter tubes offer extended service lifespans, especially under stable operational parameters. In continuous-flow applications, average replacement intervals range from 12 to 36 months depending on chemical exposure and cleaning frequency.
Lifecycle management involves monitoring parameters such as permeability loss, pressure drop, and fouling index. Preventive maintenance combined with periodic bubble point testing extends operational life and reduces unplanned downtime.
A summary of lifecycle considerations:
| Lifecycle Factor | Typical Range | Maintenance Recommendation |
|---|---|---|
| Operational Lifespan | 12–36 months | Regular integrity tests |
| Cleaning Frequency | Monthly–Quarterly | Avoid thermal shock during CIP |
| Replacement Planning | Annually | Predictive scheduling via sensors |
Economic Trade-Offs Compared to Competing Materials
Compared to polymeric filters, alumina tubes incur higher upfront costs but deliver improved durability and chemical tolerance. Over a 5-year operational horizon, the lower replacement frequency offsets the higher initial price, often improving total cost of ownership qualitatively in corrosive or thermal-cycling environments — confirm on procurement RFQ; not a TCO % SLA.
Against zirconia, alumina offers moderate savings but sacrifices mechanical strength. SiC tubes, though thermally superior, require more frequent inspection due to pore variability and brittleness in specific geometries.
Notable economic considerations:
- Alumina vs. Polymer: Longer lifespan, better ROI in harsh environments.
- Alumina vs. Zirconia: Cost-effective where extreme strength isn't essential.
- Alumina vs. SiC: Favorable when thermal shocks are moderate.
VIII. Supplier Evaluation and Quality Assurance
Supplier choice for microporous alumina filter tubes should weigh process capability, QC, and lead-time reliability — not price alone. Prioritize pore/sinter evidence and drawing co-review over brochure claims.
Assessing Technical Capabilities and Certifications
Supplier evaluation should begin with a review of their ceramic processing expertise and adherence to quality certifications. ISO 9001 and ISO 14001 are often baseline indicators, but specialized testing capabilities—like pore size uniformity and sintering precision—are critical for microporous products.
Customization flexibility is another differentiator. Suppliers that offer co-design support, CAD drawing review, and rapid prototyping are better positioned to serve specialized filtration needs across sectors like petrochemicals and water treatment.
Key technical capabilities to prioritize include:
- Certification Standards: Look for ISO-compliant production lines.
- Testing Infrastructure: Pore analysis, thermal cycle resistance.
- Engineering Support: CAD integration and co-design options.
Lead Times and Supply Chain Reliability
For critical process applications, unpredictable lead times can disrupt maintenance schedules and plant operations. Standard lead times for alumina filter tubes range from 2 to 8 weeks depending on size and customization complexity. Shorter timelines are often achievable only when stock items are maintained locally or by the supplier.
Supply chain reliability is best assessed through historical fulfillment data, inventory policies, and contingency planning (e.g., dual sourcing). Global events—such as pandemic-related delays or port congestion—further highlight the importance of supplier transparency.
| Procurement Factor | Standard Range | Risk Mitigation Strategy |
|---|---|---|
| Lead Time | 2–8 weeks | Buffer stock or dual suppliers |
| Stock Availability | Batch-dependent | Regular inventory audits |
| Shipping Reliability | Variable by region | Track record + express options |
Essential Quality Tests: Bubble Point, Strength, and Fouling Resistance
Reliable suppliers perform rigorous post-production testing to verify each filter tube's performance. Bubble point testing ensures correct pore size and fluid retention behavior. Mechanical strength tests (e.g., crush or flexural) confirm integrity under operating pressure.
Fouling resistance is harder to quantify but often approximated through accelerated aging and chemical immersion tests. For high-volume procurement, quality data should be traceable via serial codes and test reports.
Tests that should be standardized include:
- Bubble Point Test: Confirms functional pore size range.
- Compressive Strength Test: Validates structural integrity.
- Fouling Resistance Simulation: Estimates long-term filtration stability.
X. Conclusion and Future Directions
As the use of microporous alumina filter tubes expands across industrial sectors, engineers need a consolidated understanding of material behavior, system integration, and supplier evaluation. This final section summarizes critical takeaways, highlights future innovations in material design, and discusses how digital tools will shape operational reliability.
Summary of Critical Engineering Takeaways
Microporous alumina filter tubes offer a compelling mix of thermal resistance, chemical stability, and controlled porosity for advanced separation tasks. Their compatibility with harsh process environments enables use in chemical plants, oil refineries, and gas purification systems.
Procurement decisions must consider pore size distribution, manufacturing quality, and total lifecycle costs. Engineers also benefit from standardized testing and supplier transparency.
To consolidate practical understanding, consider:
- Performance Determinants: Pore size, wall thickness, thermal durability
- Cost Factors: Purity, customization, production batch size
- Selection Criteria: Compatibility with media, pressure, and temperature
Advancements in Nanoporous Alumina Technologies
Next-generation microporous tubes are incorporating nanoporous layers to enhance filtration selectivity. Nanopores (≤100 nm) can target specific molecular contaminants, useful in pharmaceutical and microelectronics industries.
Research into hierarchical pore structures—combining macro-, micro-, and nanopores—has shown promise in increasing flow rates without compromising separation efficiency. These designs are often supported by additive manufacturing and surface modification technologies.
| Innovation Type | Impact on Performance |
|---|---|
| Nanoporous Layering | Increased selectivity at sub-micron scale |
| Hierarchical Porosity Design | Balanced permeability and retention |
| Surface Functionalization | Improved anti-fouling and catalytic activity |
Integration with Digital Simulation and Predictive Maintenance
Engineers are now using CFD (Computational Fluid Dynamics) to simulate fluid dynamics inside microporous tubes. These models allow optimization before physical trials, saving time and cost in system design. Simulations also support predictive maintenance by identifying stress points and fouling tendencies.
Integration with IoT systems can monitor flow resistance and pressure drops in real time, triggering alerts for cleaning or replacement. This enables predictive scheduling and reduces unplanned downtime.
Digital tools in future workflows:
- CFD Modeling: Optimizes pore structure vs. flow dynamics
- IoT Monitoring: Tracks filtration performance in real time
- Predictive Algorithms: Improve maintenance and lifecycle planning
IX. Environmental and Safety Considerations
While microporous alumina filter tubes offer process efficiency, their lifecycle—from raw material extraction to disposal—must align with modern environmental and safety expectations. Engineers are increasingly accountable not only for system performance but also for sustainability metrics. This section highlights environmental impact, handling risks, and regulatory compliance.
Environmental Impact of Alumina Tube Manufacturing
Alumina production involves mining bauxite, refining via the Bayer process, and high-temperature sintering, each contributing to carbon emissions and energy consumption. Depending on the manufacturer’s location and energy source, the carbon footprint can range from 7–12 kg CO₂ per kg of finished product.
Water usage is another environmental concern. Sintering and polishing operations require controlled water cycles, and suppliers should ideally operate closed-loop systems. Some factories now incorporate waste heat recovery to improve energy efficiency.
To evaluate environmental compliance, check for:
- Energy Efficiency Practices: Kiln insulation, heat recovery.
- Water Conservation Measures: Recycling and pH-neutral discharge.
- Raw Material Transparency: Bauxite sourcing certifications.
Handling Safety and Disposal Practices
Although alumina is chemically inert and non-toxic, microporous tubes pose risks during machining, installation, or disposal. Fine alumina dust from cutting can irritate the respiratory system. Proper PPE—such as N95 masks and sealed gloves—is essential during customization.
Disposal requires understanding of local regulations. Spent tubes from chemical processes may be classified as contaminated waste and must undergo treatment. Unused or clean tubes can often be landfilled, but crushing is recommended to prevent reuse.
| Safety Concern | Best Practice Recommendation |
|---|---|
| Dust Inhalation During Cutting | Use wet methods and full PPE |
| Post-Use Disposal | Analyze chemical residues before landfilling |
| Storage Conditions | Avoid humidity and physical stress |
Compliance with Global Sustainability Standards
Clients in the EU, Japan, and the U.S. often demand proof of compliance with environmental and sustainability frameworks such as RoHS (Restriction of Hazardous Substances), REACH (Registration, Evaluation, Authorisation and Restriction of Chemicals), and WEEE (Waste Electrical and Electronic Equipment).
For industrial filtration systems, additional compliance may include ISO 14001 environmental management systems. Suppliers that provide lifecycle analysis (LCA) or environmental product declarations (EPDs) can support ESG (Environmental, Social, Governance) reporting.
Sustainability frameworks to align with:
- RoHS & REACH: Ensure material safety and traceability.
- ISO 14001: Validates structured environmental management.
- EPD/LCA Availability: Enables client-side ESG reporting.
Conclusion
Microporous alumina filter tubes integrate precise pore structures, stable mechanical properties, and chemical resistance into a single solution for complex separation tasks. This makes them well-suited for challenging conditions like demulsification, gas purification, and catalyst support.
Long-term performance depends on selecting the right pore size, tube geometry, and supplier quality. Engineers must balance technical specifications with lifecycle cost and regulatory compliance.
To summarize the most actionable insights:
- Material Stability: ~1100–1200 °C oxidizing screening — confirm on grade sheet + duty
- Filtration Precision: Pore sizes from 0.1–10 µm as catalog-typical RFQ screening — confirm on drawing + duty
- Procurement Strategy: Lock pore·porosity·wall·media·ΔP·temperature on RFQ; see microporous filter tube, alumina tubes, and custom services
FAQ: Microporous Alumina Filter Tubes
Q1. What is the typical pore size range of a microporous alumina filter tube?
A1. Most microporous alumina filter tubes feature pore sizes in a 0.1–10 µm catalog-typical RFQ screening window — confirm on drawing + duty. Fine pores below ~1 µm are often discussed for oil-water separation and gas-phase filtration. Match pore size to the targeted particle or droplet size; do not treat page windows as a universal aperture contract.
Q2. How do microporous alumina filter tubes perform at high temperatures?
A2. These tubes are often screened for structural integrity around 1100–1200 °C under oxidizing duty — confirm on grade sheet + duty — making them candidates for hot-gas filtration or catalytic reactions when matched to process. Their α-phase alumina matrix resists phase transformation, preventing deformation or pore collapse even under thermal cycling. This performance exceeds that of polymer or metallic filters.
Q3. Are microporous alumina filter tubes resistant to acids and alkalis?
A3. Yes, microporous alumina filter tubes are chemically inert to most acids and alkalis under ambient and elevated temperatures. However, hydrofluoric acid (HF) or hot concentrated phosphoric acid may attack the alumina structure. Protective coatings or material alternatives should be considered in such cases.
Q4. What are the key quality tests during procurement?
A4. Critical tests include the bubble point test (for pore integrity), compressive strength test, and flow rate analysis. Suppliers should provide full data sheets and ISO/ASTM compliance reports. Verification through third-party labs is recommended for critical applications.
Related reading
- Advanced alumina membrane tubes for wastewater treatment — When wastewater oil-water membrane / MWCO / TMP duty dominates instead of microporous filter-tube pore/ΔP RFQ
- Alumina ceramic in petrochemical systems — When broader petrochemical alumina duty (not filter-tube pore architecture) gates material choice
- Thermal shock failure in alumina tubes for gas delivery — When dense gas-delivery tube thermal-shock risk dominates instead of intentional microporous filtration
References:
-
Sacrificial templating is a common pore-forming route in advanced ceramic fabrication. ↩
-
Interconnected micropores govern permeability and selectivity in microporous filter tubes. ↩
-
Bubble point pressure testing is a standard pore-continuity check for porous ceramics. ↩
-
Chemical stability soak tests help verify media compatibility under harsh duty — confirm protocol on RFQ. ↩